Introduction
Plasterboard waste generation
Plasterboard waste is generated during construction, refurbishment, and demolition projects. Actual amounts of plasterboard waste generated in the EU and respective Member States are unavailable, but it is estimated that 2.35 million tons of plasterboard waste are produced annually in Europe, with an extra 0.6 million tons produced during plasterboard manufacturing and installation1,2. Current plasterboard recycling plants rely on several mechanical processes, namely manual segregation, grinding, sieving, and magnetic separation, that remove paper, concrete, foam, paint, plastics, wood, ceramics, glass, and ferrous metals from gypsum. These recycling processes are almost exclusively aimed at the recovery of pre-consumer plasterboard waste, namely onsite-plasterboard offcuts3. On the other hand, post-consumer plasterboard waste from refurbishment and demolition projects has high levels of contaminants that can damage equipment in current recycling plants4, which hinder its operational recovery and recycling. This highlights the lack of suitable purification technologies for post-consumer plasterboard waste.
Post-consumer gypsum recycling
Although gypsum (CaSO4.2H2O) is a material that can be recycled indefinitely through calcination-rehydration cycles and at a lower cost than landfilling1, it must meet several requirements for plasterboard manufacturing. The British Standard Institute PAS 109 recommended CaSO4.2H2O contents in recycled gypsum of > 85 wt%5. One of the main challenges to produce recycled gypsum from post-consumer plasterboard waste is attributed to the difficulty to achieve consistent CaSO4.2H2O contents > 92 wt% via current mechanical recycling processes3. Indeed, CaSO4.2H2O content of recycled gypsum from post-consumer plasterboard waste is typically in the range 75-90 wt%6.
Water-soluble phosphorus, chloride, magnesium, sodium, and potassium salts could also be present in mechanically recycled gypsum, which migrate to the paper-gypsum interface during plasterboard drying and affect paper bonding strength4. The GtoG project established that the content of these salts in recycled gypsum should be < 0.02 wt%6, but the uncertain quantity of salt content in recycled gypsum from post-consumer plasterboard waste restricts its utilization in plasterboard manufacturing4. This was related to high water-soluble salt contents, which was ascribed to restraining residual paper in recycled gypsum3.
Acid leaching is a purification process that has been used almost exclusively for the removal of toxic heavy metals and radioactive nuclides in phosphogypsum, which is obtained as a by-product during phosphoric acid production7–13. This purification process was performed with sulfuric acid, H2SO4, because is relatively cheap and yields more gypsum after neutralization with calcium oxide or calcium carbonate14,15. Higher temperature and H2SO4 content, and longer residence time were found to increase acid leaching purification efficiency16.
Aims of this work
Our preliminary work17 was the first to demonstrate that an improved mechanical pre-treatment followed by acid leaching purification at 90 °C for 1 h using a 5 wt% H2SO4 solution can achieve purity levels > 96 wt% in gypsum from refurbishment plasterboard waste. The main aims of the current work were to (1) demonstrate that the improved mechanical pre-treatment together with the novel acid leaching purification process can produce purified post-consumer gypsum with consistent > 96 wt% purity, which is the current maximum purity in recycled gypsum3; (2) evaluate the performance of calcined purified gypsum samples (stuccos); and (3) propose an industrial-scale acid leaching purification plant design to minimize environmental and economic impacts. Two approaches for post-consumer gypsum purification were evaluated: i) acid leaching purification followed by filtration, washing, and drying, to maximize the efficiency of the acid leaching purification process; and ii) acid leaching followed by neutralization, filtration and drying, to reduce the economic and environmental impacts of the acid leaching purification process.
Materials and methods
Plasterboard waste sourcing
Refurbishment plasterboard waste (RPW) was sourced from a household waste and recycling center in Nottingham (United Kingdom), and demolition plasterboard waste (DPW) was obtained from a recycling site in Leicester (United Kingdom). The collected refurbishment and demolition plasterboard waste samples are shown in Figure 1.
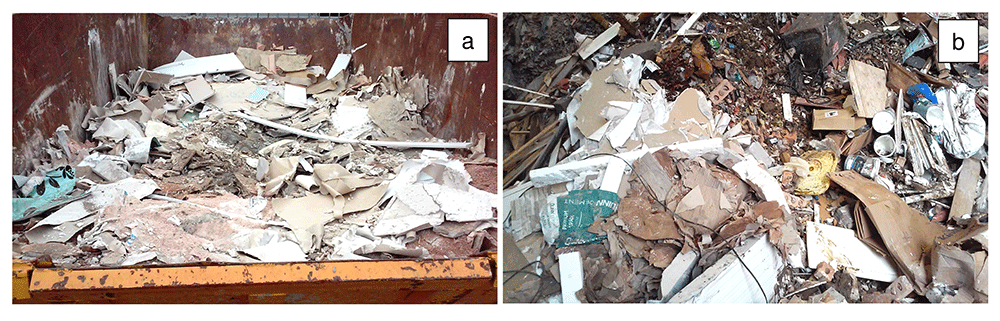
Figure 1. Plasterboard waste sample sourcing.
(a) Refurbishment plasterboard waste (RPW): household waste and recycling center, Nottingham, United Kingdom. (b) Demolition plasterboard waste (DPW): recycling site, Nottingham, United Kingdom.
Approximately 30 kg of each waste was collected in plastic bags to be transported to the laboratory. Then, the wastes were manually segregated in the laboratory to determine their total contaminant content. Contaminants comprising paper, mortar, plastics, foam, wood, and glass were found in the collected plasterboard waste samples. RPW contained 10 wt% of contaminants whilst DPW contained 23 wt% of contaminants.
Reference materials and chemicals sourcing
Mineral gypsum (MG) and commercial stucco (CS) currently used in plasterboard manufacturing were provided as fine powders by a UK plasterboard supplier. MG was used for comparison purposes and to define the criterion for the calculation of the chemical purity of the samples through X-ray fluorescence. CS was produced in a continuous calciner at 150 °C and was used as reference to evaluate stuccos obtained from gypsum from post-consumer plasterboard waste before and after acid leaching purification. Sulfuric acid (H2SO4, Fisher Chemicals, certified analytical reagent, minimum purity 95 vol%) and distilled or purified water were used to prepare the H2SO4 solutions to carry out the acid leaching tests. Calcium hydroxide powder (Ca(OH)2, Acros Organics, ACS reagent, purity > 95 wt%) was used in neutralization and wastewater treatment tests.
Post-consumer gypsum preparation
Post-consumer gypsum with particle sizes < 250 µm was prepared through crushing and sieving of refurbishment and demolition plasterboard wastes. Crushing and sieving allowed for the removal of paper fragments and fibers, and particle sizes < 250 µm were chosen to increase acid leaching purification efficiency. Two sieves with apertures of 2 mm and 250 µm and a receiver tray were used at the sieving stage. The diameter of the sieves and tray was 300 mm, and the sieves conformed to standards ISO 3310-1 and BS 410-1. Initially, RPW and DPW samples were broken down into fragments < 4 cm in size. These fragments were then crushed manually with porcelain mortar and pestle, and the crushed material was sieved to obtain < 2 mm particle sizes and remove paper fragments. Afterwards, the material passing was crushed again using the same procedure described above and sieved to obtain < 250 µm particle sizes and remove paper fibers, which represented < 0.5 wt% of the obtained post-consumer gypsum. The post-consumer gypsum obtained from refurbishment and demolition plasterboard waste samples will be referred to as GRPW and GDPW, respectively. The procedure to obtain GRPW and GDPW is displayed in Figure 2. Two batches of GRPW (1.5 kg each) and two batches of GDPW (1.5 kg each) were used as feedstocks for acid leaching purification tests. Gypsum particles < 2 mm in size obtained from refurbishment plasterboard waste were also used in one acid leaching purification test.
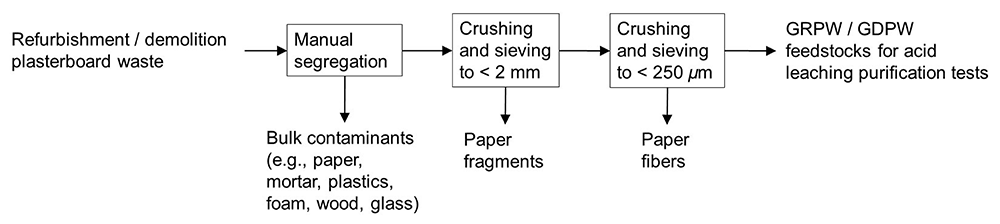
Figure 2. Schematic representation of the improved mechanical pre-treatment.
This mechanical pre-treatment produced the GRPW or GDPW feedstocks for acid leaching purification tests.
Laboratory-scale acid leaching post-consumer gypsum purification tests
In the first approach, laboratory-scale acid leaching purification tests were performed with a 500 mL Pyrex® borosilicate beaker, a hot plate, and a Camlab OS20-S LED digital overhead stirrer with a PTFE-coated crossed stirrer shaft. Tests were conducted with 100 g of either GRPW or GDPW, a gypsum/solution ratio of 1:3 wt/wt that was found optimum for acid leaching phosphogypsum purification8, a gypsum slurry volume of 350 mL, and a stirring speed of either 50 or 150 revolutions per minute (rpm). Temperatures of 24 °C, 60 °C and 90 °C, H2SO4 contents of 3 wt% (0.3 M), 5 wt% (0.5 M) and 10 wt% (1.1 M), and residence times of 30 min, 1 h, 1.5 h, 2 h and 3 h were evaluated. GRPW and GDPW were added to the H2SO4 solution at room temperature and the acidic gypsum slurry was heated to the target temperature at a rate of 3–4 °C/min. The temperature of the acidic gypsum slurry was monitored with an independent thermocouple. At the end of the test, the slurry was allowed to cool down to room temperature and the purified post-consumer gypsum was recovered using a Buchner filtration kit connected to a vacuum pump. Distilled or purified water was used to wash the purified post-consumer gypsum cake. Cake washing was carried out until the color of litmus paper in contact with the filtrate indicated pH 6. Then, the purified post-consumer gypsum cake was dried in an oven at 45 °C for either 12 or 24 h depending on its water content. Drying was done at 45 °C to prevent conversion of gypsum (CaSO4.2H2O) into stucco (CaSO4.½H2O). Finally, the dried sample was crushed with ceramic mortar and pestle to produce a fine powder.
In the second approach, acid leaching purification was carried out with < 2 mm gypsum particles, stirring speed of 50 rpm and 3 wt% H2SO4 solution, and the acidic gypsum slurry was neutralized to pH 5 with Ca(OH)2 prior filtration. The aim of this second approach was to develop an industrial-scale acid leaching purification plant design. The same laboratory setup was used in acid leaching and neutralization steps. The pH was measured with a bench top Hanna Instruments pH meter (model HI-2211). The neutralized slurry was filtered to recover the purified post-consumer gypsum and the wastewater. The wastewater and a magnetic stir bar were placed in the same 500 mL borosilicate beaker used for acid leaching purification tests. The beaker was placed on the top plate of a magnetic stirrer and Ca(OH)2 powder was gradually added until a pH of 10.5 was reached. The resulting precipitate was filtered and dried at room temperature.
Experimental techniques
The chemical composition of the gypsum samples was determined through X-ray fluorescence (XRF). XRF analyses were conducted with an Orbis micro-XRF spectrometer. Pellets for XRF characterization were prepared by blending 0.8 g of gypsum powder with 0.2 g of boric acid powder (binder). Then, this blend was placed in a die and piston of 5 mm in diameter and compacted in a manual hydraulic press applying 10 tons of force. XRF data were acquired under vacuum in five regions of the pellet using a voltage of 30 kV, current of 0.4 mA, amplifier time of 1.6 µs and acquisition time of 120 s. The weight percentages of SO3, CaO, SiO2, Al2O3, Fe2O3, MnO, MgO, P2O5, K2O, Na2O, Ni2O3, SrO and Cl were recorded. Previous research identified MgO, P2O5, K2O, Na2O and Cl compounds present in gypsum as detrimental for plasterboard manufacturing4,7. MG was also used as reference to establish the methodology for the calculation of gypsum’s chemical purity through XRF. MnO content in GRPW and GDPW was higher than in MG (Table S1 in Extended data18), whereas Ni2O3 and SrO contents were mostly below the detection limit of the XRF spectrometer (< 0.1 wt%). In this work, MnO, Ni2O3 and SrO were assumed to be impurities and the chemical purity of gypsum was considered as the sum of SO3, CaO, SiO2, Al2O3 and Fe2O3 contents (Equation 1). The CaSO4 content (i.e., sum of CaO and SO3 contents) was also determined to differentiate between gypsum samples with similar chemical purity values.
Chemical purity (wt%) = SO3 + CaO + SiO2 + Al2O3 + Fe2O3 (1)
The contents of gypsum (CaSO4.2H2O), bassanite or stucco (CaSO4.½H2O), quartz (SiO2) and calcite (CaCO3) in the gypsum samples and the contents of CaSO4.2H2O, CaSO4.½H2O and anhydrous CaSO4 in the stuccos were determined through X-ray diffraction (XRD). XRD patterns were obtained using a Bruker D2 Phaser X-ray diffractometer, fitted with a 1-dimensional Lynxeye detector, and using Ni filtered Cu Kα radiation run at 30 kV and 10 mA. Patterns were recorded from 10–100° 2θ, using a step size of 0.02, and were analyzed with DIFFRAC.EVA diffraction software. ICDD-PDF numbers 74-1433, 33-0310, 83-0437, 05-0490 and 05-0586 were used for the semi-quantitative and qualitative analysis of CaSO4.2H2O, CaSO4.½H2O, CaSO4, SiO2 and CaCO3, respectively. XRD analysis of the precipitates obtained from the wastewater was also carried out. Gypsum (CaSO4.2H2O), brucite [Mg(OH)2], kieserite (MgSO4.H2O) and portlandite [Ca(OH)2] were identified and quantified using ICDD-PDF numbers 74-1433, 07-0239, 70-2156 and 04-0733, respectively.
GRPW and GDPW before and after acid leaching purification tests were characterized through thermal gravimetric analysis (TGA) and derivative thermogravimetry (DTG). MG was also characterized for comparison purposes. TGA/DTG profiles were recorded with a TA Q5000IR thermogravimetric analyzer (TA Instruments Inc., US). An amount of 20 mg was placed in a sealed aluminum pan with a pierced lid and heated from 40 °C to 250 °C using a heating rate of 5 °C/min. A nitrogen flow rate of 20 mL/min was applied to the balance throughout the test. Stoichiometrically, pure CaSO4.2H2O is constituted by 20.93 wt% of H2O. Therefore, the theoretical CaSO4.2H2O content in the gypsum samples was calculated by multiplying the weight loss at 240 °C by a factor of 4.778.
The particle size distribution of GRPW and GDPW feedstocks used in acid leaching purification tests was determined with a Malvern Mastersizer 3000 with Hydro EV dispersion unit and wet measurement cell, using isopropanol as dispersant. Five determinations were performed with each sample and average values were calculated. A Zeiss EVO 50 scanning electron microscopy (SEM) instrument was used to investigate the crystal morphology of GRPW before and after acid leaching. First, the samples were sprinkled onto a carbon tab attached to the SEM stub, and then, coated in gold to reduce charging. SEM images were acquired using a magnification of ×500.
GRPW and GDPW feedstocks and purified samples with particles < 150 µm in size were calcined at 150 °C for 1 h in a stationary oven to produce stuccos. Three 1-hour calcination steps were required to reduce the CaSO4.2H2O content in the samples to < 2 wt%. An ELE Automatic Vicat apparatus that complies with British standard EN 13279-2:2014 was used to determine the initial setting time of each stucco. A water/stucco ratio of 0.7 wt/wt that was adopted in similar studies19–22 was used. Distilled water and stucco were mixed manually for 90 s prior testing. Preliminary Vicat tests performed with 200 g, 300 g and 500 g of CS showed that good data reproducibility was only achieved when using 200 g. Then, each mixture containing 200 g of stucco was placed inside a Vicat conical ring of 40 mm in height, upper internal diameter of 60 mm and lower internal diameter of 70 mm. The Vicat conical ring was mounted on a round glass plate of 150 mm diameter and 6 mm thickness. The initial setting times were recorded when the needle was 22 mm above the glass plate (or 18 mm penetration), as specified by British standard EN 13279-2:2014. All Vicat tests were performed in triplicate and average values were calculated.
Results and discussion
Improved mechanical pre-treatment
The manual segregation step of the improved mechanical pre-treatment (Figure 2) reduced the contaminant content in batch 1 of RPW from 10 wt% to 7 wt% and in batch 1 of DPW from 23 wt% to 15 wt%. Subsequent crushing and sieving of plasterboard fragments to produce gypsum particles < 250 µm in size reduced the contaminant content in post-consumer gypsum to 4–6 wt%.
Table S1 in Extended data18 shows the chemical composition and chemical purity of the two different batches of GRPW and GDPW studied in this work and the composition of MG. The chemical purity values of batch 1 and batch 2 of GRPW calculated using Equation 1 were respectively 95.9 wt% and 94.9 wt%. Likewise, the chemical purity values of batch 1 and batch 2 of GDPW were respectively 96.0 wt% and 94.7 wt%. These results show that the difference in the chemical purity of batch 1 and batch 2 of GRPW and GDPW was 1–1.3 wt%. Moreover, the chemical purity values of these batches were comparable to that of MG (95.1 wt%). The CaSO4 contents of GRPW and GDPW (94.3 wt% and 93.2 wt%) were higher than in MG (89.9 wt%). The main impurity in GRPW and GDPW was phosphorus (P2O5 ≥ 2 wt%).
The particle size distribution profiles of GRPW and GDPW are presented in Figure 3. The particle size distribution profiles of GRPW and GDPW were similar, with the maximum particle volume densities at around 135 µm and 150 µm, respectively. The presence of particles > 250 µm in size in both samples could be due to agglomeration of gypsum particles and/or presence of non-spherical particles (e.g., paper fibers).
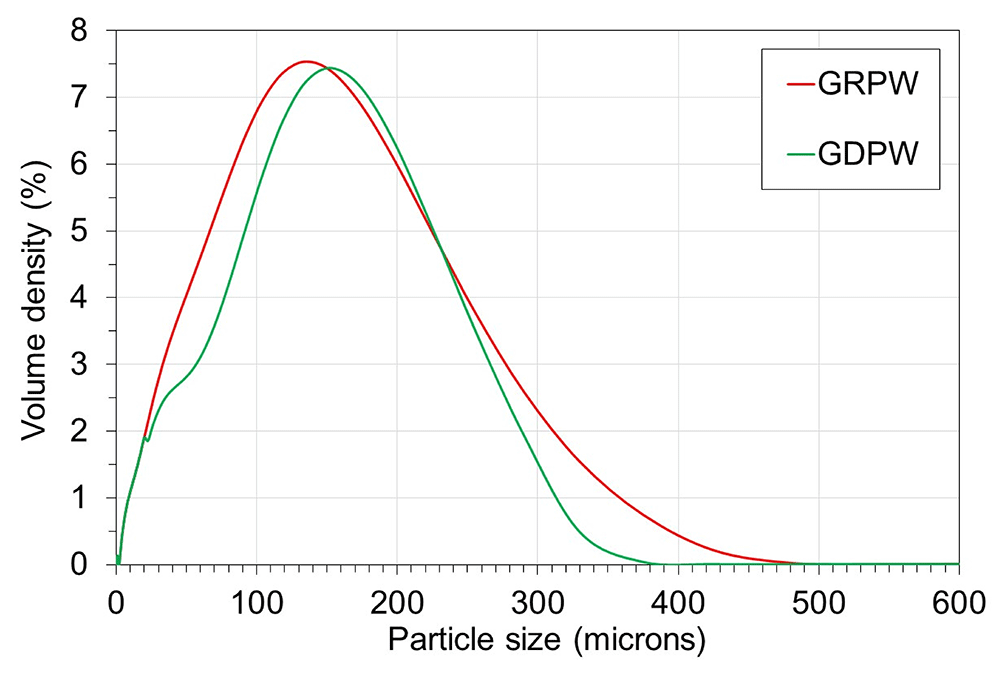
Figure 3. Particle size distribution of batch 1 of gypsum from refurbishment from plasterboard waste (GRPW) and batch 1 of gypsum from demolition plasterboard waste (GDPW) used as feedstocks in acid leaching purification tests.
Acid leaching post-consumer gypsum purification
The results from laboratory-scale acid leaching purification tests with batch 1 of GRPW and batch 1 of GDPW using different temperatures, residence times and H2SO4 contents are presented in Figures 4a and 4b, respectively. The actual data can be found in Table S2 in Extended data18.
In the case of GRPW (Figure 4a), there were no significant differences in the chemical purity of the purified samples (around 96.5 wt%) and, in general, these values were 0.5–1.0 wt% higher than that of the GRPW feedstock. These results might suggest that acid leaching purification at 60 °C for 30 min using a 3 wt% H2SO4 solution would be sufficient to produce purified GRPW with chemical purity > 96 wt%. However, the CaSO4 contents in purified gypsum were usually lower when acid leaching was performed at 60 °C than at 90 °C, which could be explained by the Ostwald ripening process. This process consists of the initial dissolution of small CaSO4.2H2O crystals followed by deposition and recrystallization of dissolved CaSO4 on the surface of larger crystals. The Ostwald ripening process was observed by Zheng et al.11 during acid leaching of a gypsum waste under hydrothermal conditions at 100–120 °C. The CaSO4 content in batch 1 of GRPW increased from 94.3 wt% in the feedstock to 95.6 wt% when acid leaching purification was carried out at 90 °C, either for 30 min using a 10 wt% H2SO4 solution or for 1 h using a 5 wt% H2SO4 solution. Therefore, it is thought that acid leaching under these conditions favored the deposition and recrystallization of dissolved CaSO4, leading to the observed increase in the CaSO4 content in purified GRPW. Under these two acid leaching conditions, no changes in P2O5, MnO, K2O and MgO contents were observed, but Na2O content decreased by 76% and Cl content decreased by 37%. Arguably, it would be preferable to perform acid leaching purification using a 5 wt% rather than a 10 wt% H2SO4 solution to minimize H2SO4 consumption.
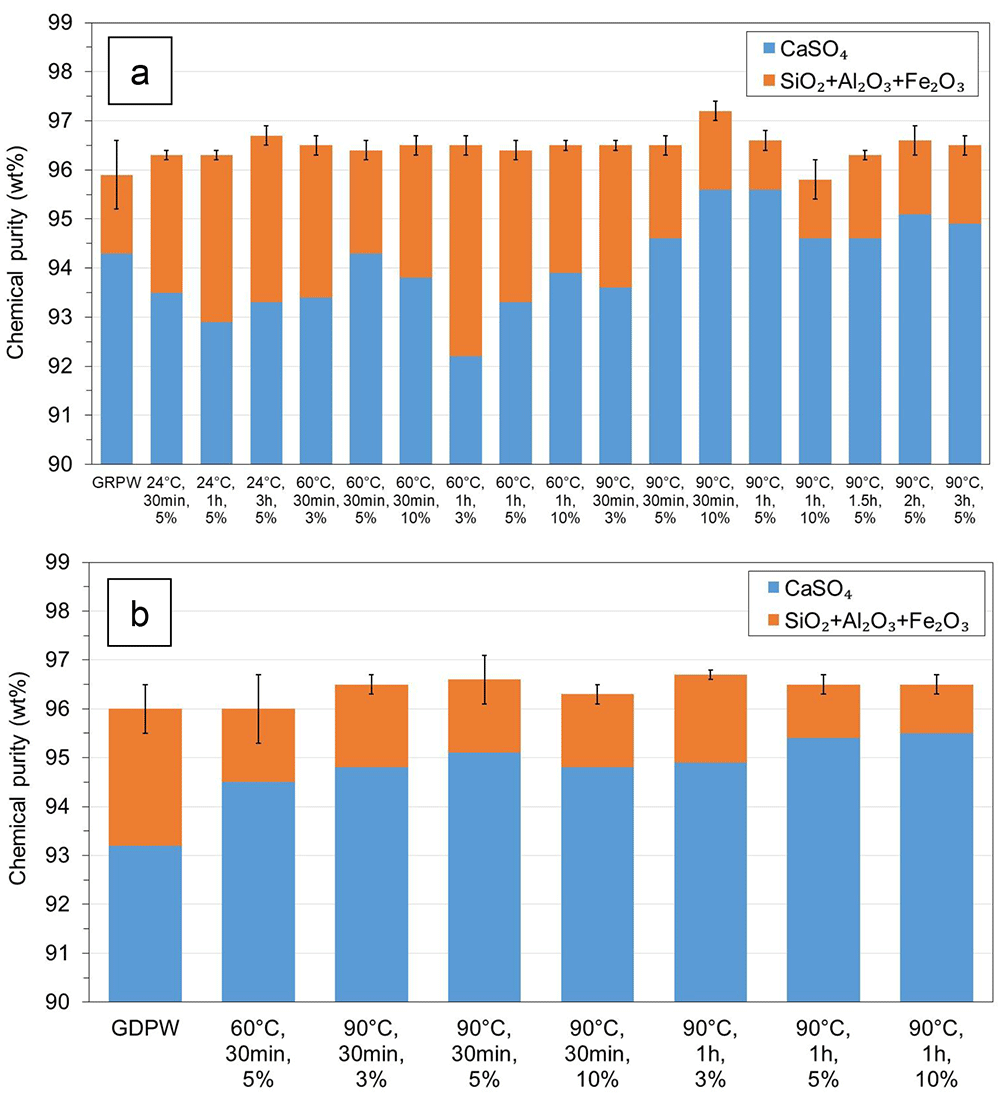
Figure 4. Chemical purity of post-consumer gypsum before and after acid leaching using different temperatures, residence times and H2SO4 contents.
(a) Batch 1 of gypsum from refurbishment plasterboard waste (GRPW). (b) Batch 1 of gypsum from demolition plasterboard waste (GDPW).
SEM images of the crystals from batch 1 of GRPW before and after acid leaching purification at 90 °C for 1 h using a 5 wt% H2SO4 solution are shown in Figure 5. GRPW feedstock appeared to be made up of agglomerations of small gypsum crystals, and acid leaching seemed to increase the gypsum crystal size. These findings concur with the hypothesis that gypsum particles underwent the Ostwald ripening process during acid leaching.
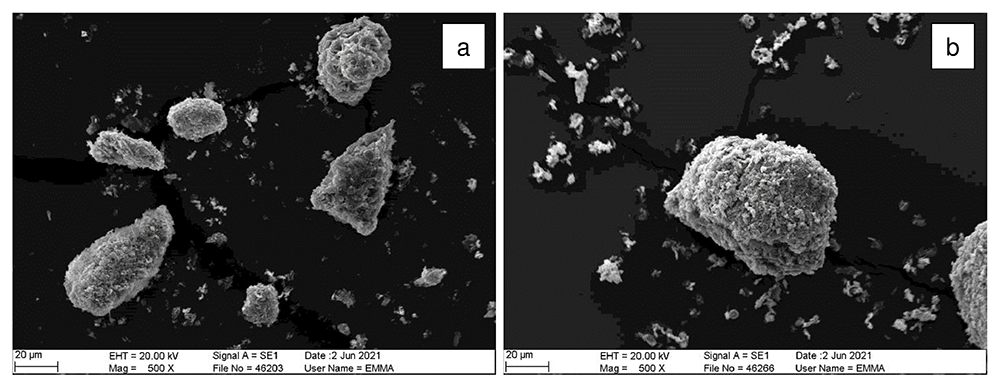
Figure 5. SEM images.
(a) GRPW feedstock. (b) GRPW after acid leaching at 90 °C for 1 h using a 5 wt% H2SO4 solution.
Taking into consideration GRPW results, most acid leaching purification tests with batch 1 of GDPW were carried out at 90 °C for either 30 min or 1 h using different H2SO4 solutions. Figure 4b shows that the chemical purity did not change significantly in treated GDPW samples and were comparable to the chemical purity in treated GRPW samples (96.5 wt%). The highest CaSO4 content of 95.5 wt% was obtained after acid leaching purification at 90 °C for 1 h using either 5 wt% or 10 wt% H2SO4 solutions. Therefore, optimum acid leaching purification conditions were 90 °C for 1 h using a 5 wt% H2SO4 solution, which resulted in an increase of 0.5–0.7 wt% in the chemical purity and an increase of 1.3–2.2 wt% in the CaSO4 content of GRPW and GDPW.
The CaSO4.2H2O content in GRPW and GDPW before and after acid leaching purification under optimum conditions of 90 °C for 1 h using a 5 wt% H2SO4 solution was determined semi-quantitatively through XRD and calculated theoretically through TGA. XRD peaks positioned at 11.6°, 20.7°, 23.4°, 29.1°, 31.1°, 33.3° and 43.3° are associated to CaSO4.2H2O, whereas peaks positioned at 14.6°, 25.6°, 29.7°, 31.7°, 32.9° and 49.1° are associated to CaSO4.½H2O23,24. The XRD spectra of all samples were dominated by the presence of CaSO4.2H2O (Figure S1 in Extended data18). Peaks associated to CaSO4.½H2O were absent in GRPW, GDPW and MG spectra. However, there were small peaks associated to CaCO3 and SiO2.
Figure 6 shows TGA and DTG results for GRPW and GDPW before and after acid leaching purification under optimum conditions. Acid leaching purification increased the weight loss in GRPW and GDPW by around 0.5 wt%, which could be attributed to the removal of chemical impurities and increase in CaSO4 content compared to the feedstocks (Figures 4a and 4b). The first devolatilization peak at around 135 °C in the DTG profiles (peak 1) is associated to water removal from CaSO4.2H2O as it converts into CaSO4.½H2O. The second devolatilization peak (peak 2) corresponds to water removal from CaSO4.½H2O to produce anhydrous CaSO4. The DTG profiles of GRPW and GDPW show only small differences.
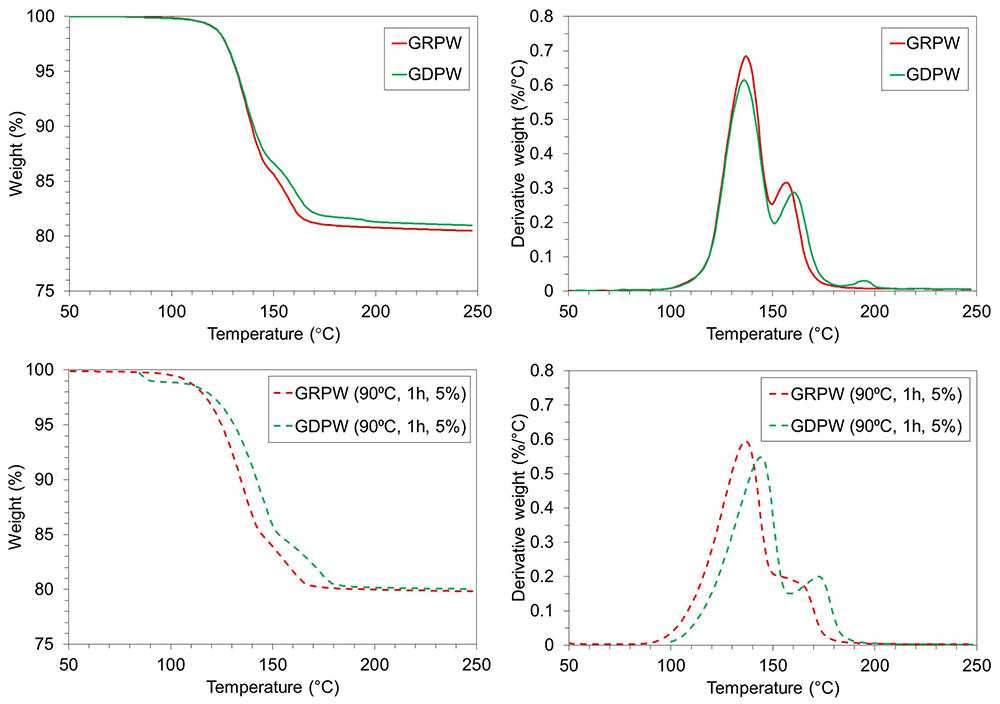
Figure 6. TGA and DTG profiles.
Batch 1 of gypsum from refurbishment plasterboard waste (GRPW) and batch 1 of gypsum from demolition plasterboard waste (GDPW) before (top) and after (bottom) acid leaching at 90 °C for 1 h using a 5 wt% H2SO4 solution.
The CaSO4.2H2O content in GRPW and GDPW before and after acid leaching purification under optimum conditions was determined with XRD and TGA data (Table 1). The CaSO4.2H2O content in GRPW and GDPW determined through XRD was usually higher than that calculated from TGA data. This could be rationalized by the impact of paper fibers in TGA results.
Table 1. Mineral composition and CaSO4.2H2O content calculated respectively through XRD and TGA for batch 1 of GRPW and batch 1 of GDPW before and after acid leaching purification at 90 °C for 1 h using a 5 wt% H2SO4 solution.
| Sample | XRD | TGA |
|---|
CaSO4.2H2O
(wt%) | CaSO4.½H2O
(wt%) | SiO2
(wt%) | CaCO3
(wt%) | CaSO4.2H2O
(wt%) |
|---|
| GRPW (feedstock) | 95 | Trace | 1 | 4 | 93 |
| GRPW (purified) | 98 | Trace | 1 | 1 | 96 |
| GDPW (feedstock) | 91 | 4 | 1 | 4 | 91 |
| GDPW (purified) | 97 | Trace | 2 | 1 | 95 |
XRD data show that acid leaching purification increased the CaSO4.2H2O content of GRPW and GDPW above 96 wt%, and decreased the CaCO3 content, as it reacted with H2SO4 to produce CaSO4.2H2O and CO2 (Equation 2). Therefore, it is thought that the increase in CaSO4.2H2O content was not only caused by the removal of impurities but also by the reaction of CaCO3 with H2SO4.
CaCO3(s) + H2SO4(l) + H2 O(l) → CaSO4.2H2 O(s) + CO2(g) (2)
TGA data show a 3–4 wt% increase in CaSO4.2H2O content in GRPW and GDPW after acid leaching purification. Acid leaching purification of GDPW did not produce purified post-consumer gypsum with > 96 wt% CaSO4.2H2O content mainly because the CaSO4.2H2O content in the GDPW feedstock was low (91 wt%). TGA results suggest that the improved mechanical pre-treatment of post-consumer plasterboard waste must produce GRPW and GDPW with > 92 wt% CaSO4.2H2O content for the acid leaching purification process to be effective and produce purified post-consumer gypsum with > 96 wt% CaSO4.2H2O content.
Overall, the CaSO4.2H2O content of GRPW and GDPW feedstocks ranged between 91–95 wt% and the CaSO4.2H2O content of purified GRPW and purified GDPW was ≥ 96 wt% when the CaSO4.2H2O content of the feedstocks was > 92 wt%. In addition, most CaCO3 present in GRPW and GDPW feedstocks reacted with H2SO4 to produce CaSO4.2H2O (Equation 2).
Properties of stuccos from post-consumer gypsum
The composition, water demand and initial setting times of the stuccos from batch 2 of GRPW (S-GRPW) and batch 2 of GDPW (S-GDPW) before and after optimum acid leaching purification conditions were determined (Table 2). The results for the commercial stucco (CS) and the stucco obtained from MG (S-MG) are also presented for comparison purposes. The stuccos from purified GRPW and GDPW had CaSO4.½H2O contents between 68.7 wt% and 71.8 wt%, which were comparable to that of CS (68.5 wt%) but much higher than that of S-MG (64.1 wt%). The initial setting times of the stuccos from purified GRPW and GDPW were also similar to that of CS (4 min and 40 s), whereas the initial setting time of S-MG was shorter (4 min). The long setting time of the stucco obtained from the GRPW feedstock (12 minutes) could be due to its low CaSO4.½H2O content (59 wt%) and/or high anhydrous CaSO4 content (39.1 wt%) compared to the other stuccos. However, further research would be required to get a better understanding of this finding, which is outside the scope of this work. A water/stucco ratio of 0.7 wt/wt was used with CS and S-MG. However, a water/gypsum ratio of 1.2 wt/wt was required to achieve normal consistency with S-GRPW and S-GDPW before and after acid leaching purification. Pedreño-Rojas et al.25 found that calcination at 150 °C for 3 h of a gypsum waste powder converted CaSO4.2H2O into CaSO4.½H2O but required a water/plaster ratio of 1.0 wt/wt, which was higher than the 0.55 wt/wt ratio of a commercial plaster. Bumanis et al.26 also found that mechanically recycled gypsum from construction and demolition plasterboard waste had higher water demand than a commercial gypsum. The water demand of the stuccos from purified GRPW and GDPW could be reduced with a retardant such as citric acid27. Alternatively, the calcination conditions could be optimized to reduce the water demand of these stuccos28. Optimization of the calcination conditions would be preferable since citric acid is expensive and was found to impact the compressive strength of hardened gypsum plaster27,29.
Table 2. Composition, water demand and initial setting times of the commercial stucco (CS), stucco from the mineral gypsum (S-MG) and stuccos from batch 2 of gypsum from refurbishment plasterboard waste and batch 2 of gypsum from demolition plasterboard waste (S-GRPW and S-GDPW) before and after acid leaching at 90 °C for 1 h using a 5 wt% H2SO4 solution.
| Sample | CaSO4.2H2O
(wt%) | CaSO4.½H2O
(wt%) | CaSO4
(wt%) | Water/stucco
ratio (wt/wt) | Initial setting
time (mm:ss) |
|---|
| CS (reference 1) | 2.0 | 68.5 | 29.5 | 0.7 | 04:40 |
| S-MG (reference 2) | 2.3 | 64.1 | 33.6 | 0.7 | 04:00 |
| S-GRPW (feedstock) | 1.9 | 59.0 | 39.1 | 1.2 | 12:00 |
| S-GRPW (purified) | 1.2 | 71.8 | 27.0 | 1.2 | 04:25 |
| S-GDPW (feedstock) | 2.0 | 63.2 | 34.8 | 1.2 | 04:45 |
| S-GDPW (purified) | 1.9 | 68.7 | 29.4 | 1.2 | 04:40 |
Industrial-scale acid leaching post-consumer gypsum purification plant design
An industrial-scale acid leaching purification plant design for post-consumer gypsum is proposed in this work based on the evaluation of some considerations to reduce economic and environmental impacts. These considerations were:
1. neutralization of the acidic gypsum slurry with Ca(OH)2 to pH 5 prior filtration rather than washing to avoid the use of expensive corrosion-resistant pumps and filtration equipment, reduce water consumption and prevent the precipitation of impurities;
2. stirring speed of 50 rpm rather than 150 rpm in the acid leaching step to avoid the use of expensive high-torque agitators;
3. use of gypsum particles < 2 mm rather than < 250 μm in size because the former can be easily produced with current milling equipment without the need of drying; and
4. use of 3 wt% H2SO4 solution for 2 h to reduce H2SO4 consumption in the acid leaching step and Ca(OH)2 consumption in the neutralization step.
These considerations were evaluated in the laboratory with batches 1 and 2 of GRPW (Figure 7). Batch 1 of GRPW was used to evaluate the first, second and third considerations in sequential order, and the results from the first test (washed) were obtained under optimum conditions. Batch 2 of GRPW was used to evaluate the fourth consideration using particle sizes < 250 μm at 90 °C with stirring at 50 rpm, followed by neutralization.
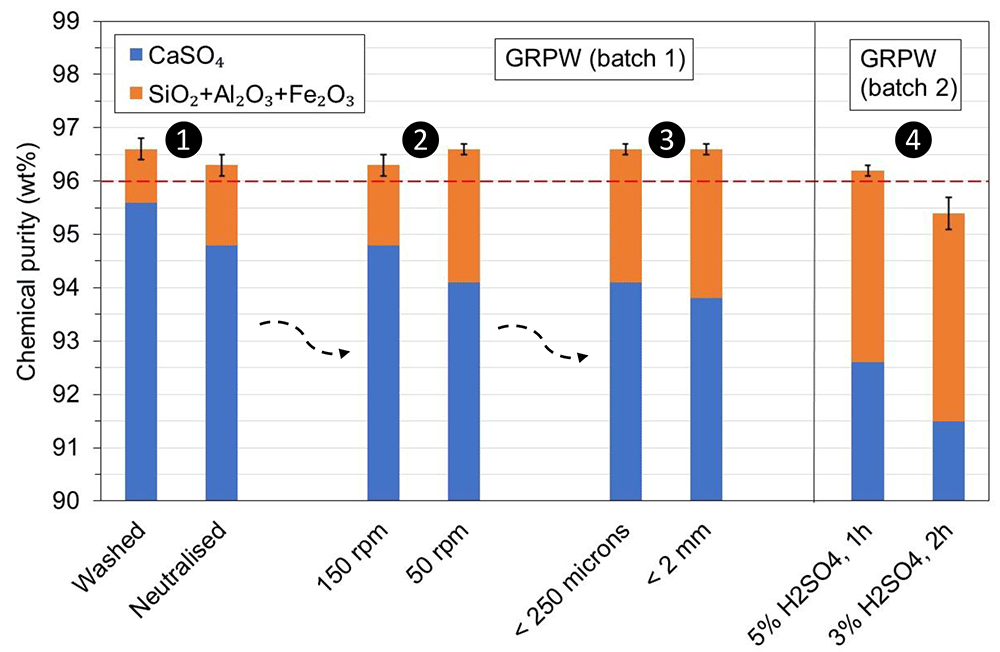
Figure 7. Chemical purity of purified batches 1 and 2 of gypsum from refurbishment plasterboard waste (GRPW) obtained with the four considerations.
The red line represents the target chemical purity value for purified post-consumer gypsum.
Neutralization of the acidic gypsum slurry to pH 5 prior filtration decreased the chemical purity of purified GRPW by 0.3 wt% and its CaSO4 content by 0.8 wt% compared to the purified GRPW obtained after washing. A reduction in the stirring speed from 150 rpm to 50 rpm increased the chemical purity of purified GRPW by 0.3 wt% but reduced its CaSO4 content by 0.7 wt%. The chemical purity was approximately 96.5 wt% regardless of whether gypsum particle sizes < 2 mm or < 250 μm were used, but the CaSO4 content decreased by 0.3 wt% with gypsum particle sizes < 2 mm. The reduction in H2SO4 content from 5 wt% to 3 wt% and increase in residence time from 1 h to 2 h decreased the chemical purity by 0.8 wt% and the CaSO4 content by 1.1 wt%. These findings suggest that only the fourth consideration would have a significant negative impact on the chemical purity and CaSO4 content of purified post-consumer gypsum. Hence, the proposed industrial-scale post-consumer gypsum purification plant design (Figure 8) consists of three processes or steps: 1) acid leaching; 2) neutralization; and 3) filtration. It is envisaged that the integration of this acid leaching purification plant in current plasterboard waste recycling sites will increase capital costs (e.g., gypsum milling equipment, storage tanks, reaction tanks, filter press, pumps) and operating costs (e.g., energy for agitator, pumps and heating system, sulfuric acid, calcium hydroxide). On the other hand, post-consumer plasterboard waste recycling through the acid leaching purification process would eliminate landfilling, increase circularity of new plasterboards, and reduce mineral gypsum extraction and consumption. From an economic standpoint, the recovery and valorization of soluble impurities in the process wastewater could compensate for the operating costs of the acid leaching purification plant. In laboratory-scale trial tests, the pH of the wastewater obtained after neutralization was raised from 5 to 10.5 with the addition of Ca(OH)2. Magnesium-rich gypsum constituted by 79.0–87.7 wt% CaSO4.2H2O, 5.2–8.9 wt% magnesium hydroxide, Mg(OH)2, 6.1–9.6 wt% magnesium sulfate dihydrate, MgSO4.2H2O, and 1.0-4.0 wt% Ca(OH)2 was precipitated. This magnesium-rich gypsum would be classified as an inorganic secondary nutrient fertilizer and could be commercialized as a source of Ca and Mg for oil palm growth and as soil ameliorant30–32. From an environmental standpoint, CO2 would be produced by reaction of H2SO4 with the CaCO3 from contaminants such as Portland cement33. The maximum CaCO3 content in GRPW and GDPW was 4 wt% (Table S1 in Extended data18). Using Equation 2, the theoretical amount of CO2 that would be produced is 17.6 kg per ton of gypsum processed. Considering that gypsum represents 95 wt% of standard plasterboards34–36, 16.7 kg of CO2 would be generated per ton of plasterboard processed. On the other hand, increasing the post-consumer plasterboard waste recycling rate from 0 to 93.6% would cause a reduction of 0.22 kg CO2 equivalent per m2 of plasterboard37. These authors noted that the density of standard plasterboards varies from 8.4 kg/m2 to 10.0 kg/m2. Hence, amounts of 22.0–26.2 kg CO2 would be avoided per ton of plasterboard processed, which are higher than the 16.7kg of CO2 generated from CaCO3. However, life cycle costing and life cycle assessment would be required to estimate the total cost and CO2 emissions from the acid leching purification plant, which are outside the scope of this work.
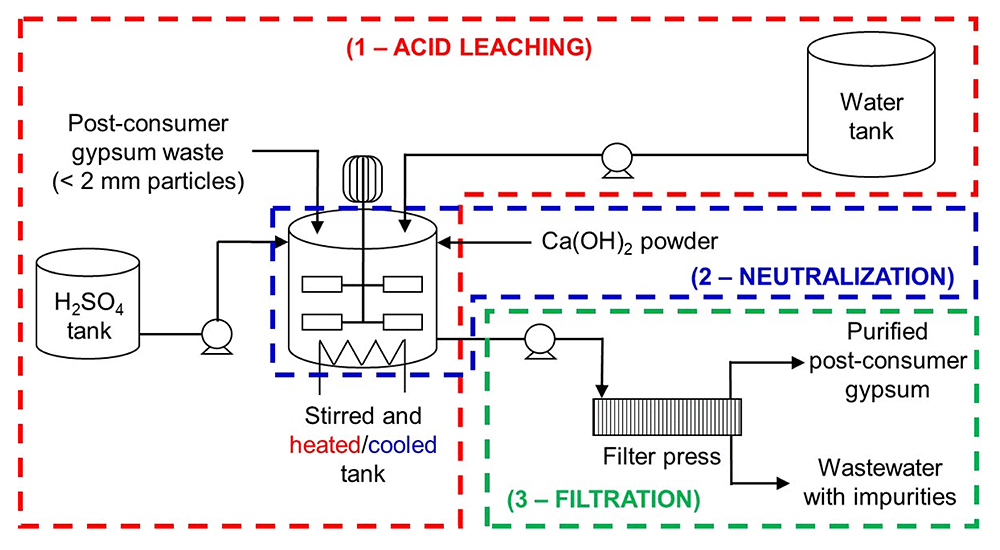
Figure 8. Proposed industrial-scale post-consumer gypsum purification plant design.
The plant consists of three processes: acid leaching, neutralization and filtration.
Conclusions
The main aims of this work were to develop an acid leaching purification process to achieve consistent chemical purity and CaSO4.2H2O contents of > 96 wt% in post-consumer gypsum; evaluate the performance of stuccos from purified post-consumer gypsum; and propose an industrial-scale acid leaching purification plant design to minimize environmental and economic impacts. Two approaches for post-consumer gypsum purification were evaluated, the first one aiming to maximize the purity level of the purified post-consumer gypsum, and the second one aiming to minimize economic and environmental impacts of the purification process. The main findings are summarized below.
1. The two-step crushing and sieving methodology of the improved mechanical pre-treatment for post-consumer plasterboard waste, first to obtain gypsum particles < 2 mm in size and then to obtain gypsum particles < 250 µm in size, was very effective to remove paper fragments and fibers and produce gypsum with chemical purity > 95.5 wt% and CaSO4.2H2O content that ranged between 91–95 wt%.
2. The posterior acid leaching purification of post-consumer gypsum (< 250 µm particles) at optimum conditions of 90 °C for 1 h using a 5 wt% H2SO4 solution produced purified post-consumer gypsum with chemical purity and CaSO4.2H2O content > 96.5 wt%.
3. The initial setting times of the stuccos obtained after calcination of purified samples at 150 °C for 3 h were similar to that of a commercial stucco but had higher water demand, which could be reduced by optimizing the calcination conditions.
4. The proposed industrial-scale acid leaching purification plant for post-consumer gypsum considered gypsum particles < 2 mm in size, stirring speed of 50 rpm and an acid neutralization step prior filtration to reduce the economic and environmental impacts of the process.
The combination and implementation of the improved mechanical pre-treatment and the novel acid leaching purification process developed in this work offers for the first time an effective purification technology for post-consumer gypsum waste, that will allow for higher recycled gypsum content in new plasterboards and the avoidance of post-consumer plasterboard waste landfilling. Future work will develop an optimum wastewater treatment process to maximize the recovery of impurities and produce water that can be reused in the acid leaching purification process.
Data availability
Underlaying data
Zenodo Digital Repository: Dataset for publication “Acid leaching technology for post-consumer gypsum purification”. https://doi.org/10.5281/zenodo.827946418.
This project contains the following underlying data:
– Dataset description.txt (abbreviations and codes of samples presented in the publication).
– Particle size analysis.zip (particle size distribution data files for the two acid leaching feedstocks in .txt format).
– SEM.zip (scanning electron microscopy images of gypsum from refurbishment plasterboard waste before and after acid leaching in .jpg format).
– TGA.zip (thermal gravimetric analysis raw data for gypsum from refurbishment and demolition plasterboard wastes before and after acid leaching in .xlsx format).
– XRD.zip (X-ray diffraction data files for samples presented in the publication in .raw, .brml and .uxd formats).
– XRF.zip (X-ray fluorescence data files for samples presented in the publication in .xlsx format).
Extended data
Zenodo Digital Repository: Dataset for publication “Acid leaching technology for post-consumer gypsum purification”. https://doi.org/10.5281/zenodo.827946418.
This project contains the following extended data:
Data are available under the terms of the Creative Commons Attribution 4.0 International license (CC-BY 4.0).
Acknowledgements
The authors would like to acknowledge the use of XRF, XRD and TGA facilities within the Loughborough Materials Characterization Centre (LMCC) at Loughborough University.
Faculty Opinions recommendedReferences
- 1.
Jiménez-Rivero A, García-Navarro J:
Indicators to measure the management performance of end-of-life gypsum: from deconstruction to production of recycled gypsum.
Waste Biomass Valori.
2016; 7: 913–927. Publisher Full Text
- 2.
Gálvez-Martos JL, Styles D, Schoenberger H, et al.:
Construction and demolition waste best management practice in Europe.
Resour Conserv Recycl.
2018; 136: 166–178. Publisher Full Text
- 3.
Jiménez-Rivero A, García-Navarro J:
Characterization of quality recycled gypsum and plasterboard with maximized recycled content.
Mater de Construccion.
2017; 67(328): e137. Publisher Full Text
- 4.
Papailiopoulou N, Grigoropoulou H, Founti M:
Techno-economic impact assessment of recycled gypsum usage in plasterboard manufacturing.
J Remanuf.
2019; 9: 141–167. Publisher Full Text
- 5.
BSI: PAS 109: Specification for the production of reprocessed gypsum from waste plasterboard. BSI Standards Limited, 2013.
- 6.
GtoG: Protocol of action B2.2: Quality criteria for recycled gypsum, technical and toxicological parameters. LIFE11 ENV/BE/001039. 2016.
- 7.
Rashad AM:
Phosphogypsum as a construction material.
J Clean Prod.
2017; 166: 732–743. Publisher Full Text
- 8.
Moalla R, Gargouri M, Khmiri F, et al.:
Phosphogypsum purification for plaster production: A process optimization using full factorial design.
Environ Eng Res.
2018; 23(1): 36–45. Publisher Full Text
- 9.
Gijbels K, Nguyen H, Kinnunen P, et al.:
Radiological and leaching assessment of an ettringite-based mortar from ladle slag and phosphogypsum.
Cem Concr Res.
2020; 128: 105954. Publisher Full Text
- 10.
Ennaciri Y, Zdah I, Alaoui-Belghiti HE, et al.:
Characterization and purification of waste phosphogypsum to make it suitable for use in the plaster and the cement industry.
Chem Eng Commun.
2020; 207(3): 382–392. Publisher Full Text
- 11.
Zheng J, Li J, Ling L, et al.:
Crystal regulation of gypsum via hydrothermal treatment with hydrogen ion for Cr(VI) extraction.
J Hazard Mater.
2020; 390: 120614. PubMed Abstract
| Publisher Full Text
- 12.
Mukaba JL, Eze CP, Pereao O, et al.:
Rare earths’ recovery from phosphogypsum: An overview on direct and indirect leaching techniques.
Minerals.
2021; 11(10): 1051. Publisher Full Text
- 13.
Haneklaus N, Barbossa S, Basallote MD, et al.:
Closing the upcoming EU gypsum gap with phosphogypsum.
Resour Conserv Recycl.
2022; 182: 106328. Publisher Full Text
- 14.
Tu YJ, Chang CK, You CF, et al.:
Recycling of Cu powder from industrial sludge by combined acid leaching, chemical exchange and ferrite process.
J Hazard Mater.
2010; 181(1–3): 981–985. PubMed Abstract
| Publisher Full Text
- 15.
Jha MK, Lee JC, Kim MS, et al.:
Hydrometallurgical recovery/recycling of platinum by the leaching of spent catalysts: A review.
Hydrometallurgy.
2013; 133: 23–32. Publisher Full Text
- 16.
Tayibi H, Choura M, López FA, et al.:
Environmental impact and management of phosphogypsum.
J Environ Manage.
2009; 90(8): 2377–2386. PubMed Abstract
| Publisher Full Text
- 17.
Castro-Díaz M, Osmani M, Cavalaro S, et al.:
A methodologic approach based on hydrocyclone separation and acid leaching to purify gypsum from refurbishment plasterboard waste. Proceedings of Sardinia 2021 - 18th International Waste Management and Landfill Symposium. CISA Publisher,
2021. Reference Source
- 18.
Castro-Díaz M, Osmani M, Cavalaro S, et al.:
Dataset for publication “Acid leaching technology for post-consumer gypsum purification”.
Zenodo Digital Repository.
2023. http://www.doi.org/10.5281/zenodo.8279464
- 19.
Erbs A, Nagalli A, Carvalho KQ, et al.:
Properties of recycled gypsum from gypsum plasterboards and commercial gypsum throughout recycling cycles.
J Clean Prod.
2018; 183: 1314–1322. Publisher Full Text
- 20.
Pereira VM, Camarini G:
Evaluation of dehydration temperature on properties of recycled gypsum plaster.
Key Eng Mater.
2016; 668: 275–282. Publisher Full Text
- 21.
Pinheiro SMM, Camarini G:
Characteristics of gypsum recycling in different cycles.
Int J Engin Tech.
2015; 7(3): 215–218. Publisher Full Text
- 22.
Erbs A, Nagalli A, Mymrine V, et al.:
Determination of physical and mechanical properties of recycled gypsum from the plasterboard sheets.
Ceramica.
2015; 61: 483–487. Publisher Full Text
- 23.
Azdarpour A, Asadullah M, Junin R, et al.:
Direct carbonation of red gypsum to produce solid carbonates.
Fuel Process Technol.
2014; 126: 429–434. Publisher Full Text
- 24.
Geraldo RH, Pinheiro SMM, Silva JS, et al.:
Gypsum plaster waste recycling: A potential environmental and industrial solution.
J Clean Prod.
2017; 164: 288–300. Publisher Full Text
- 25.
Pedreño-Rojas MA, Flores-Colen I, De Brito J, et al.:
Influence of the heating process on the use of gypsum wastes in plasters: Mechanical, thermal and environmental analysis.
J Clean Prod.
2019; 215: 444–457. Publisher Full Text
- 26.
Bumanis G, Zorica J, Korjakins A, et al.:
Processing of gypsum construction and demolition waste and properties of secondary gypsum binder.
Recycling.
2022; 7(3): 30. Publisher Full Text
- 27.
Camarini G, Cavalini Pinto MC, De Moura AG, et al.:
Effect of citric acid on properties of recycled gypsum plaster to building components.
Constr Build Mater.
2016; 124: 383–390. Publisher Full Text
- 28.
Pedreño-Rojas MA, De Brito J, Flores-Colen I, et al.:
Influence of gypsum wastes on the workability of plasters: Heating process and microstructural analysis.
J Build Eng.
2020; 29: 101143. Publisher Full Text
- 29.
Wang X, Sun S, Tian X, et al.:
Development of environment-friendly plastering gypsum.
IOP Conf Series: Mater Sci Eng.
2019; 484: 012048. Publisher Full Text
- 30.
EC regulation No 2003/2003: Regulation (EC) No 2003/2003 of the European Parliament and of the Council of 13 October 2003 relating to fertilisers. (accessed 29th of November 2022). Reference Source
- 31.
Commission regulation No 463/2013: Commission regulation (EU) No 463/2013 of 17 May 2013 amending Regulation (EC) No 2003/2003 of the European Parliament and of the Council relating to fertilisers for the purposes of adapting Annexes I, II and IV thereto to technical progress. (accessed 29th of November 2022). Reference Source
- 32.
Ayanda AF, Jusop S, Ishak CF, et al.:
Utilization of magnesium-rich synthetic gypsum as magnesium fertilizer for oil palm grown on acidic soil.
PLoS One.
2020; 15(6): e0234045. PubMed Abstract
| Publisher Full Text
| Free Full Text
- 33.
Winters D, Boakye K, Simske S:
Toward carbon-neutral concrete through biochar-cement-calcium carbonate composites: a critical review.
Sustainability.
2022; 14(8): 4633. Publisher Full Text
- 34.
British Gypsum’s Gyproc Wallboard Environmental Product Declaration. (accessed 27th of February 2023). Reference Source
- 35.
Knauf’s Wallboard, Baseboard and Plank Environmental Product Declaration. (accessed 27th of February 2023). Reference Source
- 36.
Siniat’s GTEC Plasterboard Environmental Product Declaration. (accessed 27th of February 2023).
- 37.
Jiménez-Rivero A, Sathre R, García-Navarro J:
Life cycle energy and material flow implications of gypsum plasterboard recycling in the European Union.
Resour Conserv Recycl.
2016; 108: 171–181. Publisher Full Text








