1. Introduction
Silicon is a crucial material in European industries, and its production is of great significance to many countries. Traditionally, silicon has been produced by reducing silica with carbon in submerged arc furnaces (SAF)1. However, the aluminothermic reduction process proposed by the SisAl Pilot project2,3 presents a more environmentally friendly alternative, as it eliminates the need for raw carbon materials, thereby lowering CO2 emissions. The SisAl Pilot project is exploring this method to produce decarbonized silicon while also recycling aluminum from dross and scrap. This process can be carried out in different types of furnaces, including electric arc, induction, and rotary kilns. The last type is considered in this study, namely, a gas rotary furnace placed at Fundiciones Rey (FRey) facilities in Spain.
In the aluminothermic reduction process, the SisAl reaction mechanism takes place:
As a result of the aluminothermic reduction, Si and CaO – Al2O3 slag are obtained, and they need to be separated to obtain the purest possible silicon. The main goal of this work was to estimate the time required for both fluids to completely separate after the end of the aluminothermic reduction. To achieve this objective, the separation process was mathematically modelled according to the Navier-Stokes equations and adequate multiphase flow models. Then, numerical simulations of the separation process were carried out under various scenarios, including different initial conditions, material properties, and multiphase models.
This paper is organized as follows. In Section 2, the methodology followed through this work is presented, including a description of the industrial problem, the geometry of the rotary furnace and the physical properties of the materials involved. The proposed mathematical model is also described. Section 3 presents the main numerical results. Finally, in Section 4, conclusions regarding the obtained results are presented.
2. Methods
In this section, the methodology followed in this work is detailed. More precisely, the industrial problem related to the aluminothermic reduction in the rotary kiln and the mathematical modelling proposed to estimate the separation time are described.
Problem description
The gas rotary furnace considered in this study is made of a cylindrical steel vessel lined with a thick refractory coating, which rolls around its axial direction following two turned rings that act as guides. To enhance the mixing and homogenize the temperature of the partially molten materials, the furnace can be rotated using an electrical motor. A longitudinal view of the furnace and its main dimensions are shown in Figure 1.
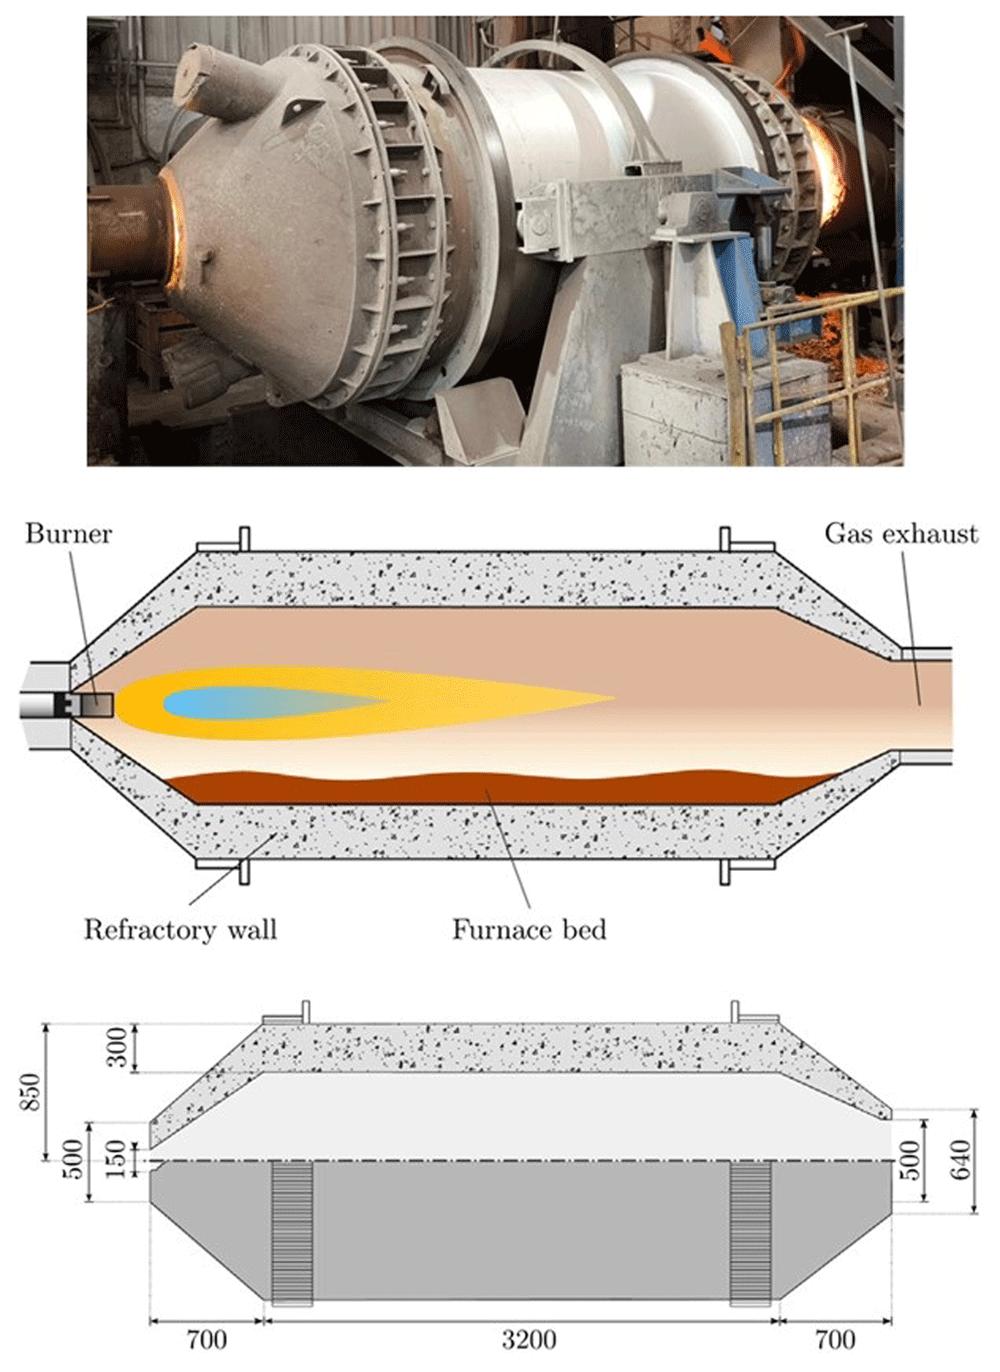
Figure 1. Rotary furnace at FRey (top), schematic diagram (center) and dimensions in mm (bottom).
During operation, on one side of the furnace, the exhaust gas collection hood remained open, and the opposite side was closed with a lid that included an oxy-fuel burner in its center. The burner injected natural gas and oxygen to generate an intense flame. The furnace can be tilted to facilitate the loading of the solid material and discharge of the melted material once the melting process is completed.
The simulation of the separation time assumes that the aluminothermic reduction has finished; therefore, neither combustion inside the furnace nor slag melting were considered in this process. Once the reaction had ended, a multiphase flow with two fluids, Si and CaO – Al2O3, was considered, and their evolution over time was analyzed.
First, the geometry of the load in the rotary furnace was determined. This is the computational domain of the simulation, which mainly depends on the inclination angle of the furnace and burden volume. The two possible rotation movements of the furnace during operation are depicted in Figure 2.
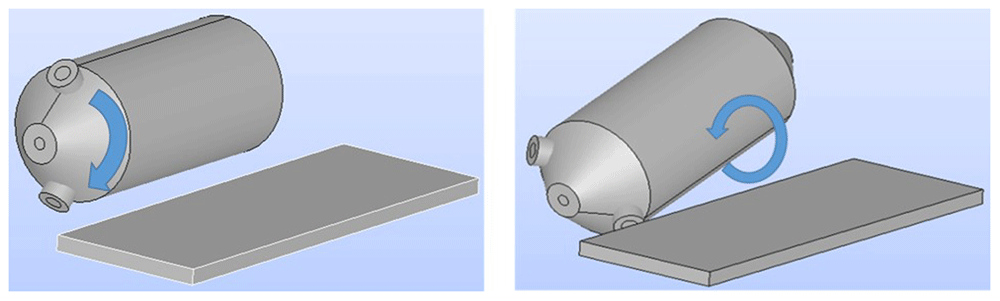
Figure 2. Possible rotation movements of the rotary furnace.
To determine the position of the charge, the relevant rotation angle was measured with respect to the horizontal plane, as the rotation along the largest furnace dimension was not considered. Thus, once the rotation with respect to the horizontal plane and burden volume are given, the geometry of the charge can be obtained. Note that the computational domain is the charge inside the furnace, not including air or the furnace itself, as shown in Figure 3.
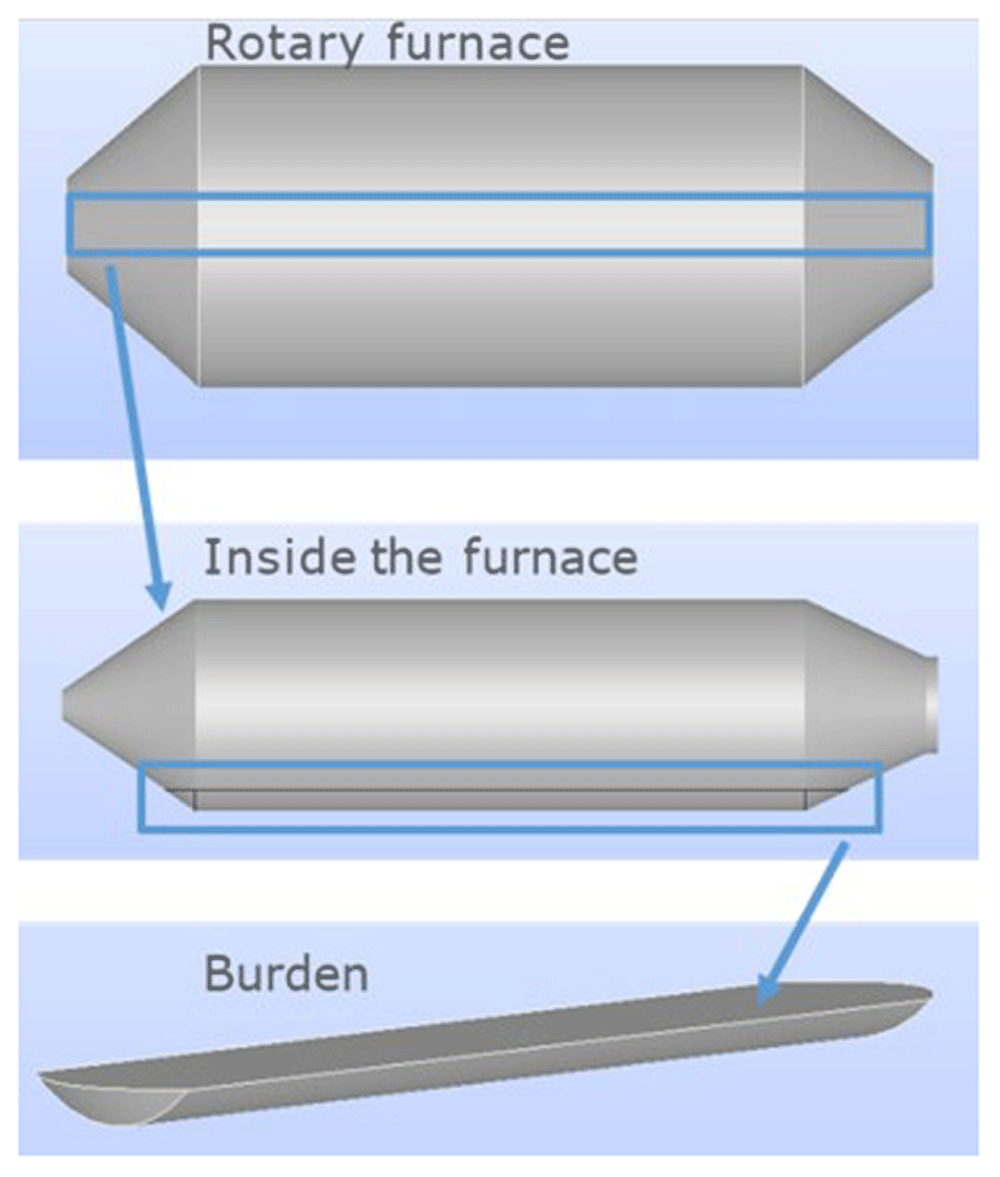
Figure 3. Location of the computational domain inside the rotary furnace.
Several charge geometries for different rotation angles are shown in Figure 4. The charge geometry used in the simulations corresponded to an inclination of 5°.
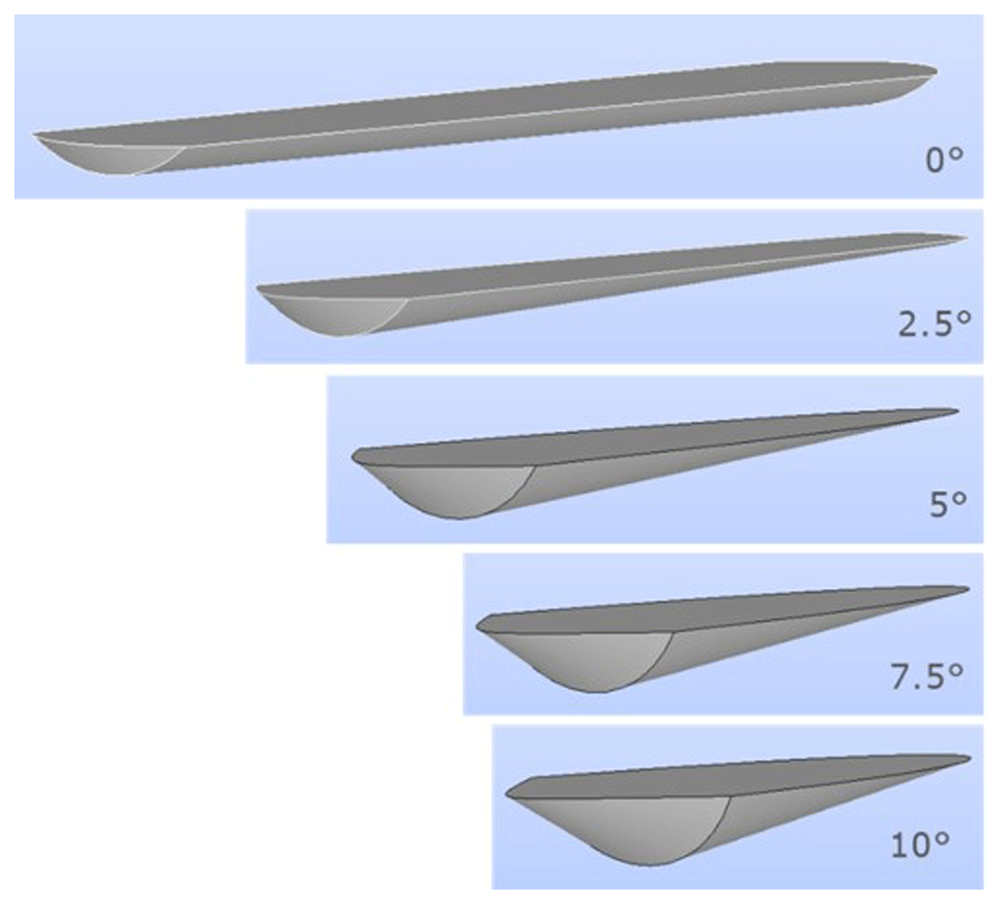
Figure 4. Charge geometry depending on the rotation angle for a given burden volume.
In principle, a 3D simulation considering Si, CaO – Al2O3 and air is desirable; however, the computational cost makes it unaffordable. The problem can be modelled, in a very good approximation, by a 2D model and by only considering the geometry of the charge corresponding to Si and CaO – Al2O3 in a longitudinal cut of the 3D domain. The proposed 2D computational domain and corresponding finite volume mesh for an inclination of 5° are shown in Figure 5.
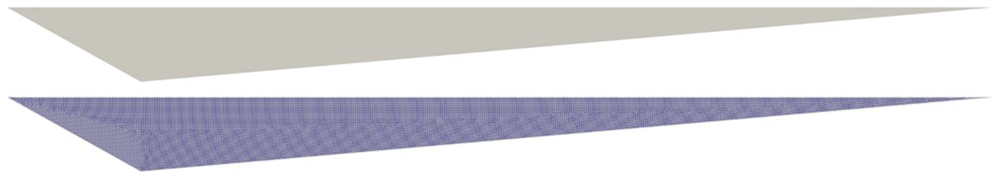
Figure 5. Computational domain (top) and mesh (bottom).
The physical properties needed for Si and CaO – Al2O3 are density and viscosity, which are summarized in Table 1.
Table 1. Densities and viscosities considered for Si and CaO – Al2O3 in the simulations.
| Si | CaO – Al2O3 |
|---|
| Density, ρ (kg m-3) | 3240 | 2500 |
| Viscosity, μ (Pa s) | 5.82E-4 | 0.1353 |
Note that both the density and viscosity of the silicon were modified to account for the fact that the furnace is commonly used to melt iron at FRey facilities; therefore, the final slag composition would be contaminated by iron adhering to the furnace walls.
Mathematical modelling
The separation problem within the charge domain was modelled using a transient hydrodynamic model. Specifically, the averaged Navier-Stokes equations and the K – ω SST turbulence model are considered in addition to an adequate multiphase flow model. The mass and momentum conservation equations are given by:
where v is the fluid velocity, p is the pressure, μT is the turbulent viscosity, D(v) is the symmetric part of the velocity gradient, and I is the identity tensor.
Moreover, the K – ω SST turbulence model4,5 involves two additonal equations for the turbulent kinetic energy, K, and the specific rate of dissipation, ω:
In the previous equations, represents the generation of turbulence kinetic energy due to mean velocity gradients, Gω represents the generation of ω; YK and Yω represent the dissipation of K and ω; ΓK and Γω represent the effective diffusivity of K and ω; and Dω is the cross-diffusion term.
With respect to the boundary conditions, zero-shear stress was considered on the top free surface, and no-slip conditions were considered on the walls.
In addition to the conservation equations and turbulence modelling, an adequate multiphase model is required to properly model the separation of both fluids. There are two main multiphase models that use different mathematical descriptions: the VOF model (see 6) and the Eulerian model. The VOF model can handle several immiscible fluids by solving a single set of momentum equations and by tracking the volume fraction of each fluid throughout the domain. On the other hand, the Eulerian option can also model several fluids but the momentum and continuity equations are considered for each phase separately. The VOF model is suitable for flows with a clearly defined phase interface, as both phases are non-interpenetrating and cannot be mixed. In contrast, the Eulerian model assumes that the two continuous phases form an interpenetrating continuum.
As a first approach, the VOF model is considered because its complexity and computational cost are less expensive than those of the Eulerian model. The general idea is to consider the initial distribution of Si and Al2O3 on the charge, simulate the evolution of both fluids until they are conveniently separated, and determine the time required to reach the final state. After this time, a denser fluid should be placed at the bottom of the charge.
3. Numerical results
The proposed model was solved using commercial software ANSYS Fluent 2022 R27. It employs a cell-centered finite volume method to discretize the conservation equations. The coupling of the velocity and pressure was achieved using the SIMPLE iterative algorithm. Least-squares cell-based schemes are considered to handle the diffusive terms, whereas second-order upwind schemes are utilized for the treatment of convective terms. Pressure interpolation was performed using PRESTO! scheme. Time discretization was performed using a second-order implicit scheme. For a more in-depth understanding of these numerical schemes, interested readers are encouraged to refer to 8 for further details.
Before the 2D resolution of the hydrodynamic model, a 3D test was considered only for demonstration purposes (see Figure 6). As expected, several weeks of computational time were required to advance only a few seconds of real-time simulation, despite the poor meshing considered.
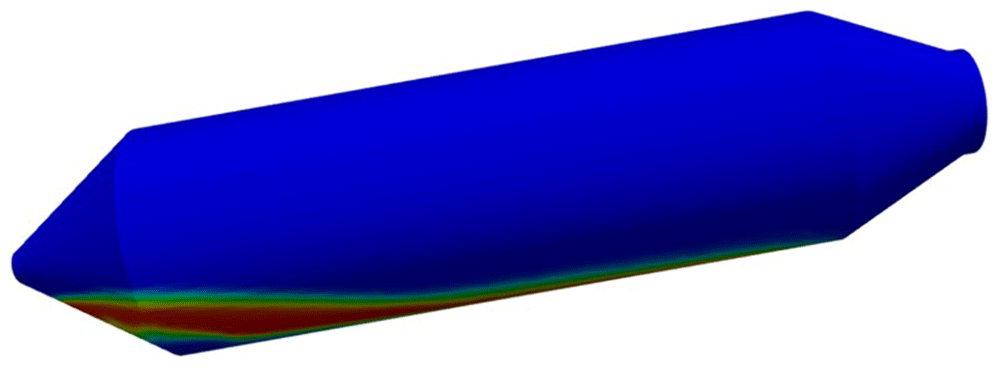
Figure 6. 3D simulation, including air, Si and CaO – Al2O3 slag, which is computationally unaffordable.
Different scenarios were considered for the 2D simulations with respect to the multiphase flow model, material properties, and initial configurations of both fluids in the computational domain. The cases addressed in this study are summarized in Table 2.
Table 2. Characteristics of the different scenarios considered.
| Scenario | Multiphase
model | Initial configuration | Material properties |
|---|
| Case 1 | VOF | Horizontal separation (Si on top) | Table 1 |
| Case 2 | VOF | Vertical separation | Table 1 |
| Case 3 | VOF | Horizontal separation (Si on top) | μ = 3.45 Pa s (CaO-Al2O3) |
| Case 4 | VOF | Horizontal separation (Si on top) | μ = 3.45 × 10⁻⁴ Pa s (CaO-Al2O3) |
| Case 5 | Eulerian | Horizontal separation (Si on top) | Table 1 |
| Case 6 | Eulerian | Homogeneous mixture | Table 1 |
| Case 7 | Eulerian | Homogeneous mixture | ρ = 2570 kg m-3 (Si); ρ = 2600 kg m-3 (CaO-Al2O3) |
First, the least favorable initial condition for the VOF model is considered, with a denser fluid (Si) on top at the initial time of the simulation, as shown in Figure 7.
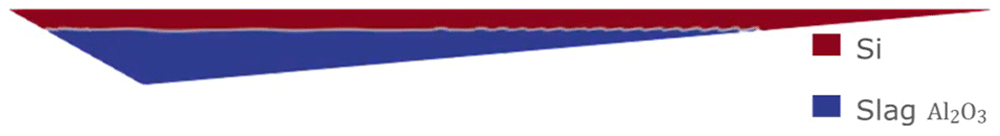
Figure 7. Case 1: initial configuration with Si on top.
The evolution of the simulation with the previous initial condition is shown in Figure 8, giving rise to a complete separation after 30 s.
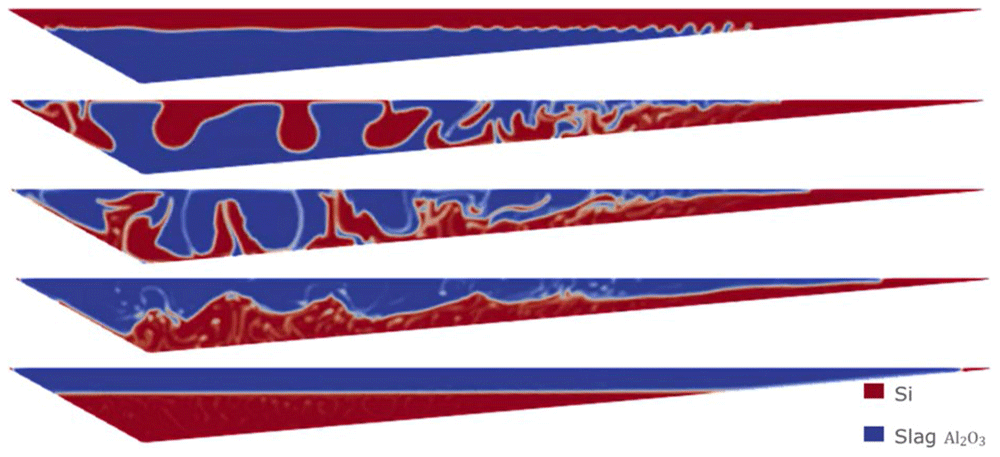
Figure 8. Case 1: complete separation after 30 s (bottom image).
Different initial conditions can be considered, for instance, a vertical initial separation between the two fluids, as depicted in Figure 9.

Figure 9. Case 2: initial configuration with vertical separation.
Although the initial condition is different from that of Case 1, the evolution of the simulation ends with a complete separation after 30 s, as shown in Figure 10.
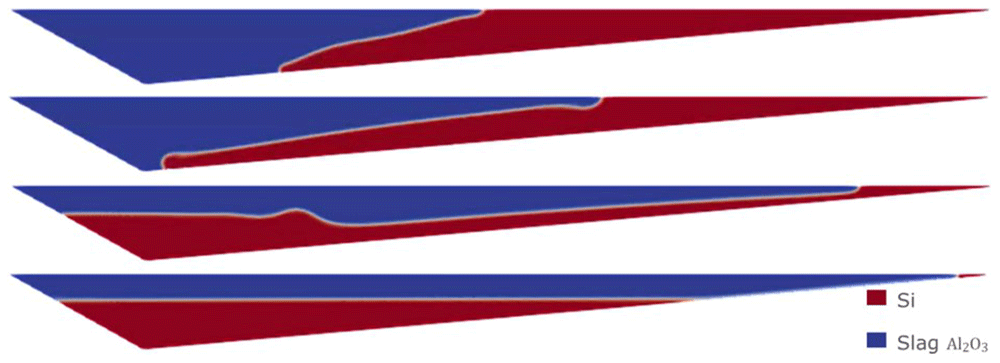
Figure 10. Case 2: complete separation after 30 s (bottom).
Sensitivity analyses were performed using the VOF model. In particular, starting from the least favorable initial condition (the same as in Case 1), extreme values for slag CaO – Al2O3 viscosity were considered, as this value is difficult to obtain from experimental measurements. In Figure 11 and Figure 12 the evolution for both Case 3 and Case 4 is shown, where different values of the slag CaO – Al2O3 viscosity were considered.
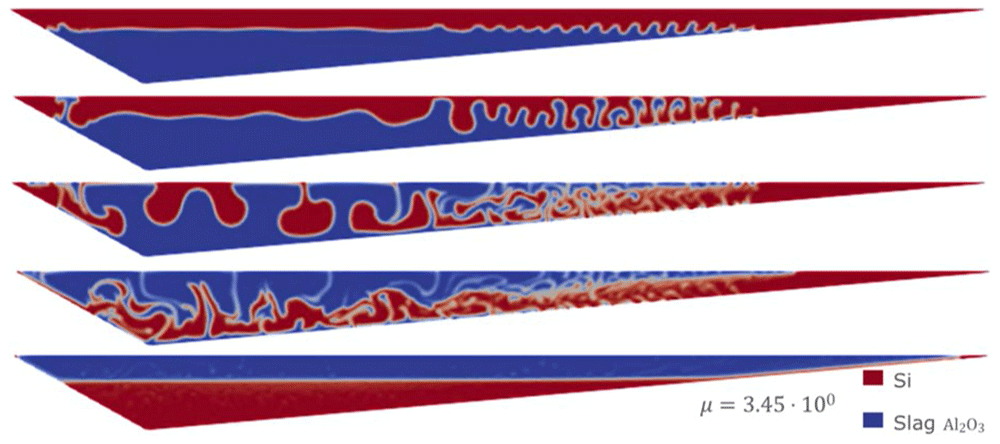
Figure 11. Case 3: complete separation after 30 s (bottom) for μslag = 3.45 Pa s.
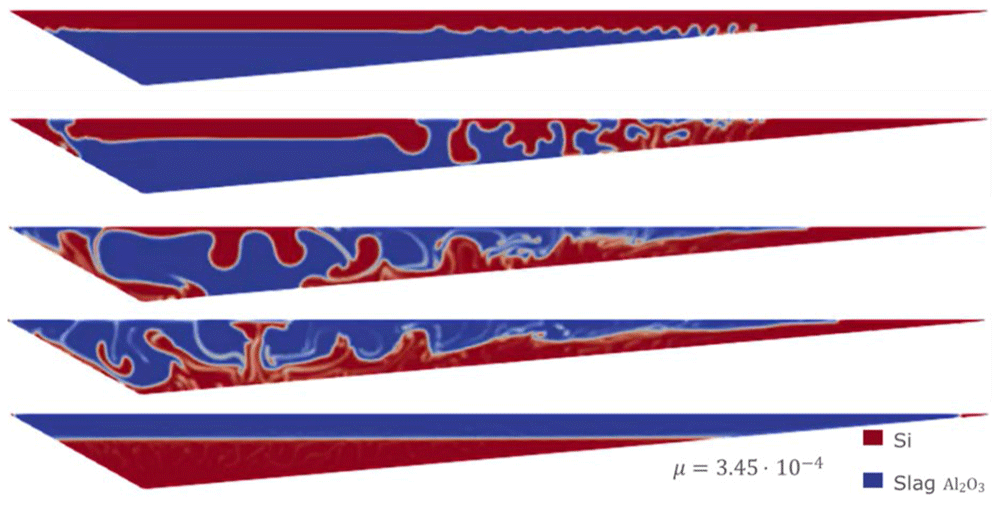
Figure 12. Case 4: complete separation after 30 s (bottom) for μslag = 3.45×10⁻⁴ Pa s.
It is observed that in all the simulations carried out with the VOF model, both Si and CaO – Al2O3 are fully separated after 30 s, regardless of the initial conditions or viscosities. Because this separation time is much shorter than the expected time for this type of process, we will change the multiphase VOF model for the Eulerian model.
Therefore, we consider the horizontal initial condition of Case 1, but for the Eulerian model, where the denser fluid (Si) is on top at the initial time of the simulation. The evolution of the separation of the two fluids is shown in Figure 13. After 30 min of simulation, the two fluids were almost completely separated.
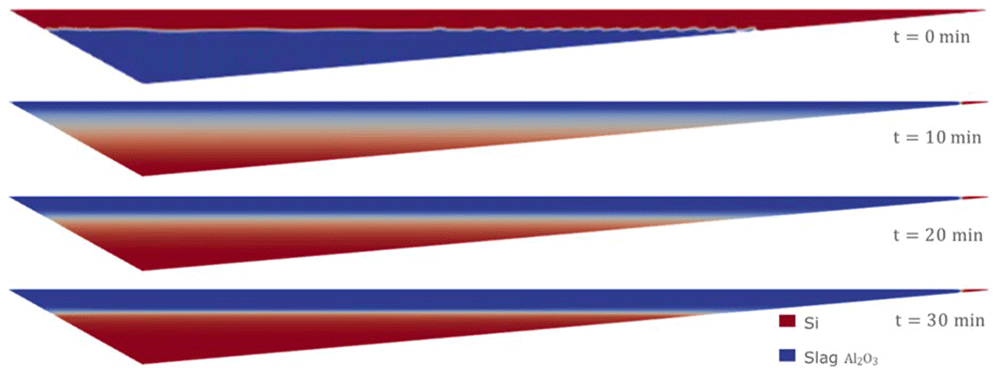
Figure 13. Case 5: complete separation after 30 min (bottom).
Moreover, using the Eulerian model, it is possible to consider an initial homogeneous mixture of Si and CaO – Al2O3. This is probably the most realistic and unfavorable initial condition for the separation process, and it cannot be considered when employing the VOF model. The evolution of the separation under this initial condition is shown in Figure 14. It was necessary to wait for at least 60 min to obtain an almost complete separation between Si and CaO – Al2O3.
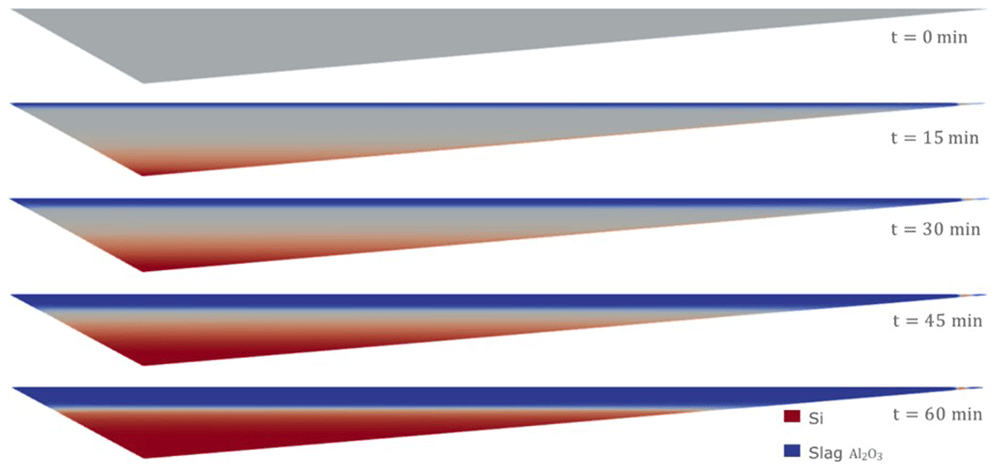
Figure 14. Case 6: complete separation after 60 min (bottom).
The separation times resulting from the Eulerian model are much higher than those obtained with the VOF model, and seem more realistic according to the knowledge obtained from the plant experience.
However, it is well known that the difference in densities between Si and CaO – Al2O3 is the key factor in controlling the separation time, which is more important than any other parameter. This can be appreciated in the following simulation using the Eulerian model, starting from the homogeneous mixture condition and with the densities of both fluids modified to 2570 kg m-3 for Si and 2600 kg m-3 for CaO – Al2O3. As shown in Figure 15, after 10 min of simulation, almost no separation was observed. This is because of the similarity of both densities, which leads to extremely long separation times.
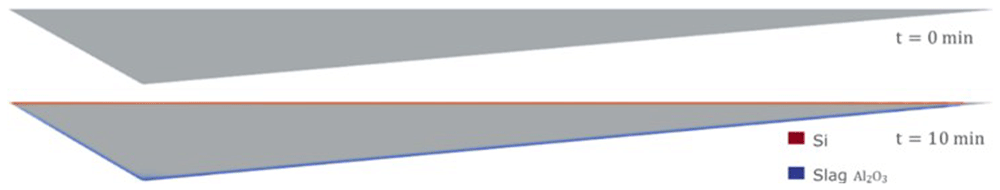
Figure 15. Case 7: no separation after 10 minutes when densities are almost equal.
4. Conclusions
Once the aluminothermic reduction process in the rotary furnace has finished, it is of industrial interest to determine how long it will take for silicon and alumina slag to separate and ensure that only silicon is cast. To meet this requirement, own code was developed to calculate the geometry of the charge inside the furnace based on its geometry, inclination, and mass of charge. After determining the geometry, a multiphase flow model was applied to estimate the separation time of the two components after the reduction process. The separation time was simulated under different conditions including different material properties, initial conditions, and multiphase models. The results obtained with the multiphase Eulerian model are more realistic than those obtained with the VOF model, which has an obvious tendency to underestimate the separation times.
As is clear from the simulations, apart from the selected multiphase flow model, the density difference between silicon and alumina slag plays a critical role in determining the separation time.
Ethics and consent
Ethics and consent were not required for this study.








