Introduction
Resilience in manufacturing policy and practice
The term resilience has regained traction in EU policy since the Covid-19 crisis and the invasion of Ukraine, ending a period of relative stability. Whereas the term resilience connects to multiple disciplines and is sometimes referred to as ‘black swan’ events, when looking at the EU policy context, we can see that it relates mainly to national (member-state) and EU-level economic abilities to respond to global shocks. On the last EU strategic agendas1,2 the chosen response to a multitude of recent crises is to intensify (twin) transitions: ‘We must make our economy more resilient and less dependent.’ This can be understood as the recognition that we need to understand the interdependence and reinforcing factors of several transitions that need to occur simultaneously. The term resilience has been put forward in a strategic foresight report from 20203 in which it is defined as ‘the ability not only to withstand and cope with challenges but also to undergo transitions, in a sustainable, fair, and democratic manner.’ When we look at where the term resilience is connected to EU policymaking, in over 70.000 occurrences on the EC Search portal, recent documents relate conflicts, disaster management, financial regulations such as the upcoming DORA regulation,4 climate change, social and economic challenges, and related policy instruments. In addition to the recently developed Resilience Dashboards by the EC,5 there are plenty of references to the Recovery and Resilience Fund (RRF), a large fund to help countries recover post Covid-19, with one of the policy goals for Member States and industries to become more resilient. The Joint Research Centre (JRC, the ECs in-house research center) has introduced Resilience Dashboards to inform policymakers and the general public on external events or developments related to resilience and it provides ‘readiness scores’ per Member State.6 These dashboards are divided into four elements: social, economic, green, digital, and geopolitical. Dashboards are based on a selection of indicators that can be categorized as capacity (enablers and/or opportunities to navigate the transitions and face future shocks) or vulnerability (obstacles or aspects that can worsen the negative impact of the challenges related to the green, digital, and fair transitions).
Figure 1 illustrates one way to measure resilience by plotting the severity of an external shock against the time a country, company, or sector is exposed to that shock. The JRC has called this ‘disturbance intensity’ versus ‘time of exposure.’ The authors propose three different stages of resilience, which represent the level of readiness to deal with shocks over time. These are stability (the ability to absorb the shock), flexibility (the ability to adapt to the shock), and change (ability to transform).
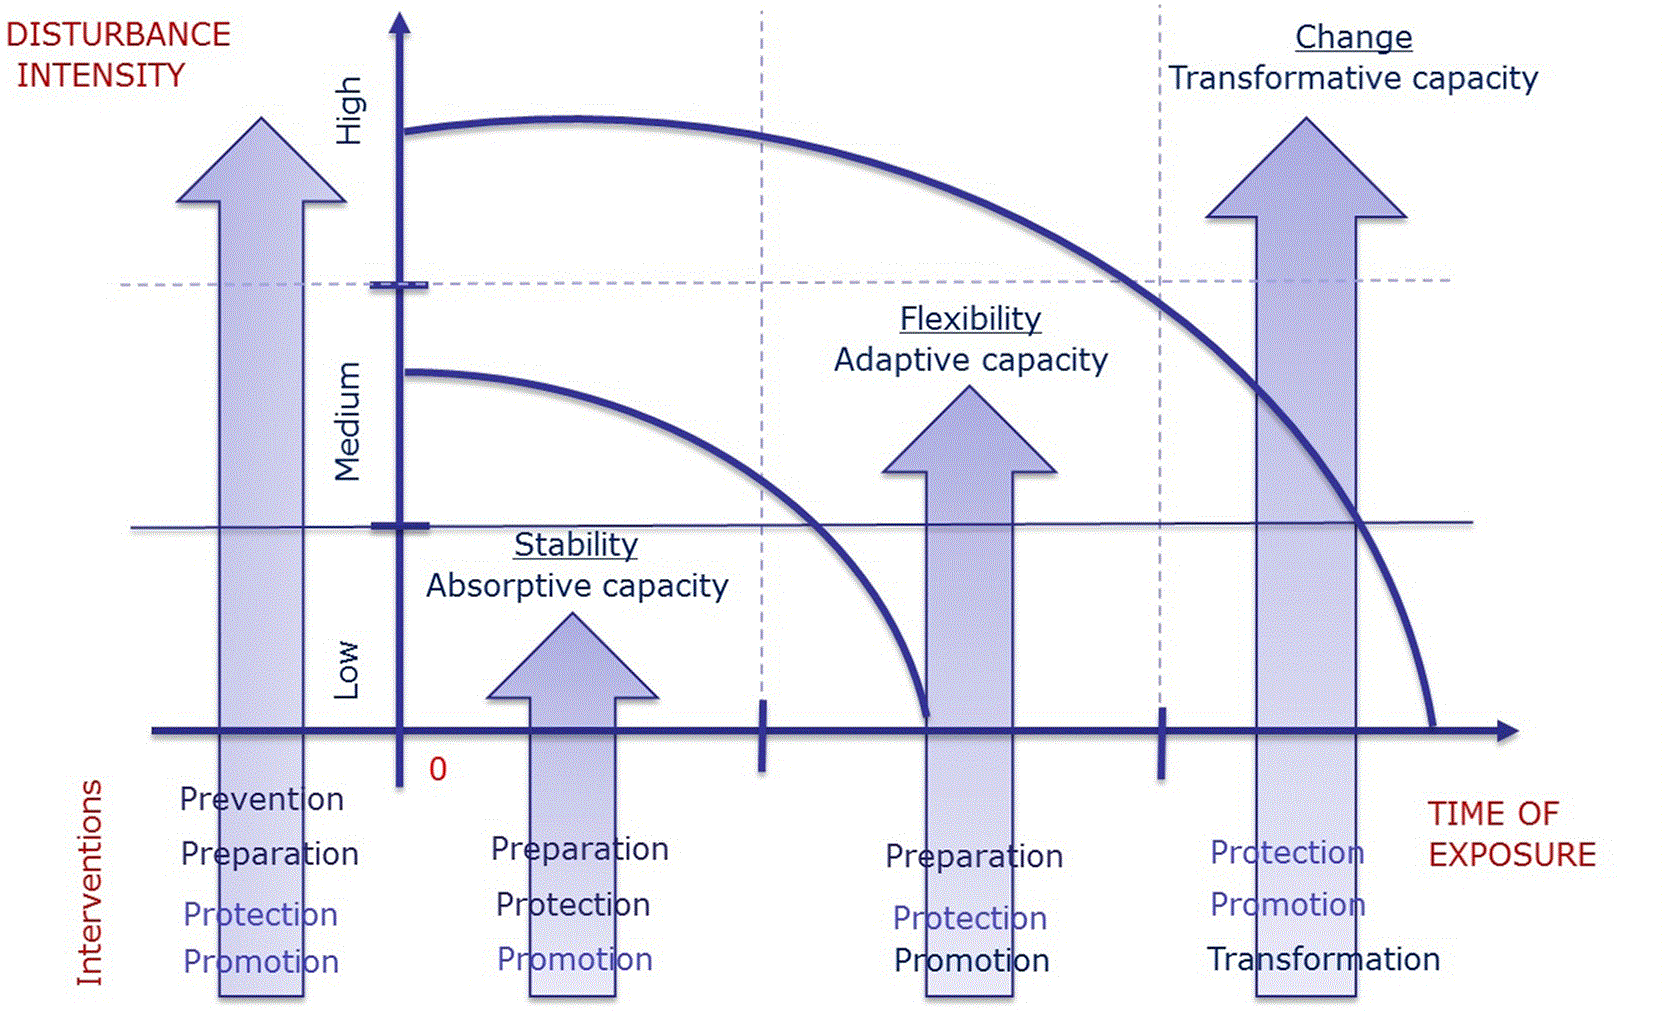
Figure 1. 3 different resilience levels.7
Taking a closer look at resilience indicators in the context of industry digitization, we see macro-economic indicators around trade (deficits in ICT-related goods and services); indicators dealing with skills, expertise, and gender balance; and indicators concerning access to and usage of ICT infrastructure, R&D investments, and e-commerce sales. Despite being developed for Member State-level analysis, the resilience self-assessment framework can serve as inspiration for the development of a framework to measure progress in resilience in manufacturing.
External disturbances, risks and resilience for manufacturing
As resilience is comprehensive and applies to multiple disciplines, the term has also found its way in the literature on manufacturing. It has become a subject of interest in supply chains and risk management procedures. In this context, resilience has been described as an adaptive capability for both expected and unexpected events. Becoming resilient is seen as a learning process and has been conceptualized8 as an ability or process rather than an outcome; it refers to a state of adaptability rather than stability.9 Moreover, it connects to vulnerability, as Sheffi and Rice (2005)10 state that ‘reducing vulnerability means reducing the chances of a disruption and increasing steps towards resilience’, paraphrased by Sohail et al. (2022).11 Likewise, the ‘made in Europe’ partnership refers multiple times to resilience for manufacturing in their strategic research agendas,12 stating that the research funded and performed under the partnership is aimed at ensuring competitiveness and sustainability, and supporting resilient and adaptive manufacturing ecosystems able to cope with external disturbances and rising environmental and social requirements, further on stating that upgradable and robust manufacturing systems and plants are necessary for flexible, responsive and resilient manufacturing. The concept of resilience is often linked to increased readiness because of a better understanding of the various types of risks. Over the last decade, the terms Volatility, Uncertainty, Complexity, and Ambiguity (VUCA) have gained traction as a way to classify external risks. Fridgeirsson et al. reported that VUCA first appeared as an acronym used by the U.S. Army War College in 1987 and became popular in strategic and leadership research throughout the 1990s.13 Fridgeirsson et al. (2021) grouped the VUCA concepts as described by Bennett and Lemoine (2014) via a set of statements14: Volatility, referring to unstable and unpredictable resource cost and/or availability at unpredictable times and durations and expected fluctuations on resources with unknown timing and magnitude. Uncertainty refers to a lack of knowledge and unclear impact of change, but the causes and effects are known. Complexity refers to the presence of many interconnected parts and often complex regulatory/political environments with multiple components. Ambiguity refers to doubt about the nature of cause and effect and the fact that little to no historical information to predict an outcome is available, making forecasting or planning difficult. A recent variation in classifying risks related to resilience strategies is that of Brittle, Anxcious, Nonlinear, and Incomprehensible (BANI).
When projecting the need for improved resilience strategies in the domain of manufacturing industries, we can crystallize such risk or disturbances and ‘plot’ them on an ideal-type production process to understand what can actually be done at the company, factory, or even workstation level to mitigate or respond to such risks. The main point of the VUCA elements therefore is to force companies or organizations to (re) think how they strategize and how they make decisions.
The study by Fridgeirsson et al. (2021)13 looks at the project level, and many studies such as the Ponomarov and Holcomb (2009),15 Matzenberger (2013),8 and Parast and Subramanian (2021),16 and the abovementioned JRC studies look at the macro-level. We want to look at sector- and company-level resilience via the VUCA elements and mitigation strategies. In this context, another term is World Class Manufacturing (WCM). Manimuthu et al. (2022) state that ‘the term has come to mean many things, but in this increasingly VUCA world (volatile, uncertain, complex, and ambiguous) WCM has to include situational understanding so that companies can seize opportunities and react quickly to threats’.17 Küpper et al. (2022), in their study on resilience and VUCA in the context of manufacturing,18 state that major global trends require producers to address three key strategic objectives, which their study participants confirmed as relevant to their operations:
• Strengthening operational resilience to address supply chain disruptions
• Improving responsiveness to changing customer requirements
• Pursuing sustainability targets
As manufacturing processes are highly dependent on materials or parts arriving on time, and leaving on time, supply chain resilience (SCR) is another important element of resilience in manufacturing. SCR refers to a supply chain system that is prepared and ready for unforeseen events and risks or uncertainties, responds to them, and can counter them (Ribeiro and Barbosa-Povoa, 201819). Supply network disruption is defined as “unplanned and unanticipated events that disrupt the normal flow of goods and materials within a supply chain.” Supply chain disruptions can stem from a wide range of possible factors, such as sociopolitical crises, natural catastrophes, and terrorism (Brüning et al., 201520; Parast & Subramanian, 202116). Being able as a manufacturing company to formulate an efficient response and build up the capability to rescue are inevitable to reduce risks and achieve resilience (Ponomarov and Holcomb, 200915). It is important to note that resilient supply chains may or may not be cost-effective in the short run, but are more capable and effective in the long run. Another recent approach to increasing resilience in the context of supply chains is ‘lean supply chain management,’ in which logic and terminology from recent ICT start-up management are brought into the manufacturing sphere.
Ito et al. (2022)9 discuss different strategies companies can adopt in facing disturbances, including building up capabilities of knowing what has happened and why, developing abilities to respond, to monitor, and to better anticipate and learn. They continue by pointing out that ‘in manufacturing companies, a commonly applied strategy for learning from past disturbances is to conduct a root cause analysis.’ While many disturbances take place on a daily basis, the severity, scale, and impact can vary widely; as such, they propose to classify disturbances by making a difference between internal and external disturbances, by level of impact, or by known-ness (new events or known issues). They point to the common stages companies adopt when facing disturbances in production: (1) detection, (2) diagnosis of the immediate cause, (3) mitigation to re-establish normal conditions, (4) root cause analysis, (5) prevention, and (6) prediction. A more comprehensive approach to resilience strategies for industry is provided by the WEF, who introduced a resilience compass displaying key strategic attention points for companies to monitor and act upon21: (1) simplified product portfolio design, (2) smart customer orientation, (3) financial visibility and agility, (4) diversified customer distribution network, (5) robust and transparent logistics, (6) responsive manufacturing setup, (7) strategic supplier relationships, and (8) advanced planning tools.
From the above lists of resilience capabilities or competences, a strong focus is placed on what companies or organizations can do once the external risk has manifested and a disturbance or disruption has taken place. However, there is an increasing need to improve forecasting, anticipation, and detection competencies as part of a resilience toolbox. Once a risk has been established, the next step is to understand the extent and timeframe in which a company can react and come up with a proper response. Such a response can play out on different levels, ranging from derisking strategies at the supply chain level to reconfiguring machines and tools on the shop floor. Ideally, lessons are learned on several levels that contribute to resilience capabilities within a company or sector. The
Figure 2 provides an organizing principle for the paper, via which we will address the different phases and connected tools, methods (solutions’) that we are developing and testing in the respective projects.
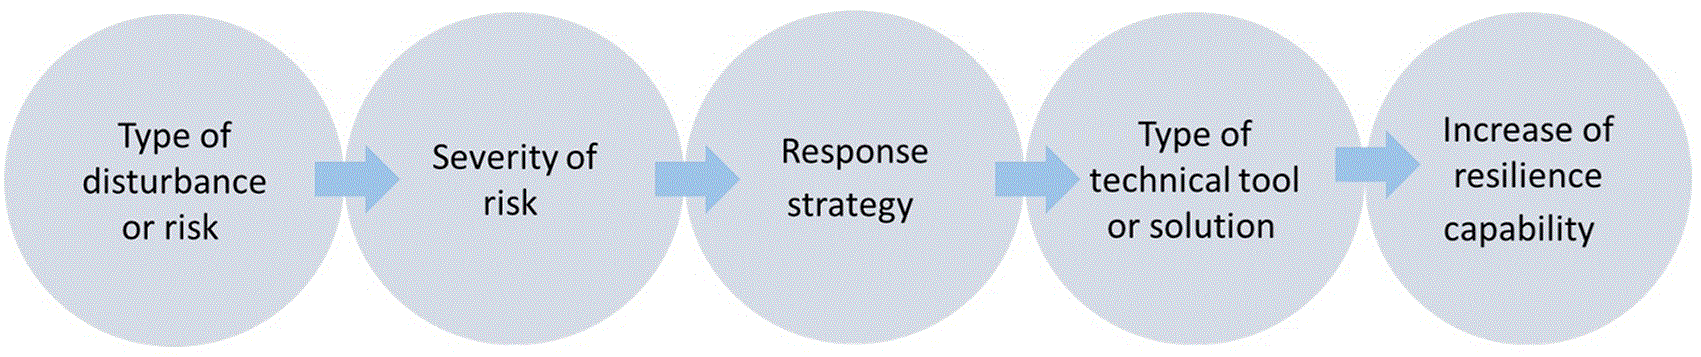
Figure 2. The ‘flow’ of resilience capability building.
In summary, in this paper, we will follow the ‘flow’ of resilience capability building and treat the different steps via examples from two ongoing research and innovation projects funded under the European HEU program. We begin by briefly introducing the projects and the industry pilot lines within these projects.
How to address resilience in practice – resilience challenges from a variety of EU industries
Addressing resilience in manufacturing through the lens of digitization
The goal of the three projects funded under the HEU program was to increase resilience via digital tools and solutions for manufacturing[1].
Flex4Res project[2] (Data spaces for flexible production lines & supply chains) focuses on achieving resilient manufacturing using advanced platform-based techniques. These techniques leverage cutting-edge technologies, including Gaia-X and International Data Spaces (IDS), to enhance data sharing across the supply chain. Central to Flex4Res is the integration of resilience assessment and reconfiguration service toolboxes, which provide critical support for identifying vulnerabilities and facilitating dynamic adjustments in manufacturing processes. Additionally, Digital Twins (DT) act as a virtual representation of the manufacturing network, enabling the effective planning and testing of reconfiguration processes before implementation. Moreover, DTs are implemented using Asset Administration Shell technology, which allows the connection of different types of data across different manufacturing assets if they have been made digital (data from machines, planning, materials, logistics, etc.). This allows manufacturers to anticipate disruptions and adjust operations accordingly. In theory, such a holistic approach complements lean management practices, improves information sharing among stakeholders, enhances coordination, and fosters adaptable and resilient manufacturing environments aligned with Industry 4.0.
In the R3 group project[3] (which stands for resilient rapid reconfigurable production process chains), the core topic is to increase resilience among industry partners by developing different digital and cyber-physical tools. These tools should help in anticipating external factors relevant to a specific market, developing strategies that make it possible to adapt and restructure internal company processes, and enabling rapid reconfiguration of production cells or larger setups. The project looks at case studies in various sectors, the common denominator being that all industry partners are European product manufacturers. Through five pilot lines, a combination of technological solutions or services should help these industrial partners improve their level of reconfigurability in the face of VUCA events. Following Industry 4.0, we discerned a set of technological pillars that need to be involved to make a digital thread possible and to allow for digital tools and services for reconfigurability to be deployed. A common platform based on the AAS will be developed to connect a wide variety of digital tools and services that will provide insights on different levels. At the workstation level, Digital Twins will enable rapid design space exploration and support optimal decision-making. At the system level, tools to support rapid reconfiguration address the logistics of the production line. At the factory level, decision-support tools will provide high-level strategic decision-making, and virtual collaborative environments will be developed to help increase workflows between product designers, material suppliers, planners, and machine engineers, while supply chain risk modelling will help in further fine-grain and tailored production capacity.
In parallel, the global objective of the RaRe2 project[4] is to create a flexible and resilient holistic ecosystem of digital tools and methodology, enabled by intensive interaction among many European organizations and projects cooperating in the rapid reconfiguration of process chains through collaborative systems and upskilling of the adaptable workforce. The key pillars of RaRe2 are as follows:
• AI-based early detection of reconfiguration needs from internal and external sources.
• Rapid adaptation of products, processes, and supply chains to change situations using digital twins.
• Empowering and upskilling humans to support decision makers in making fast, concrete decisions and quickly ramping up the workforce.
The consortium consisted of 22 European partners who developed and validated the solution in four industrial pilots and one value chain-oriented demonstrator. Therefore, the RaRe2 project develops complementary capabilities focused on the early detection of external shocks and weak signals for manufacturing SMEs. RaRe2 is a GPT-based Early Detection Tool that ingests heterogeneous external data (news, regulatory texts, market, and macroeconomic indicators) together with company-specific supply chain information. The tool is designed for SME-realistic constraints (limited labelled data, heterogeneous document formats, strict confidentiality) and is integrated into the R3GROUP toolbox structure as a macro/meso-level “front-end” service that provides early warnings and reconfiguration triggers.
The pilot line companies
R3group.
In the R3group project, there are five pilot lines (see the short descriptions in
Table 1,
Table 2,
Table 3,
Table 4 and
Table 5) in which reconfiguration is the chosen resilience approach, which focuses on digital tools and solutions, ranging from early warning systems to anticipate supply chain risks to tool-level digital twins to support rapid reconfiguration.
Table 1. Katty Fashion pilot line.
| Katty Fashion is an SME from Northeast Romania, founded in 2003, with almost 2 decades of expertise in offering bespoke services of collaborative design, product development and excellent garment manufacturing of all categories of women wears for more than 50 EU brands. |
| Goal | Facilitate sustainable product development and manufacturing through digitalization and reconfiguration. |
| Production Process | KF is already pursuing the transition from the traditional sampling process to the digital sampling process through the integration of collaborative design in a 3D environment. |
| Main challenge | The current challenge of KF is the lack of digitalization and interconnectivity of the production (horizontally and vertically), which limits the degree that the digitalization of the product development workflow can be exploited towards rapid reconfiguration. |
| Vision | To enable vertical and horizontal integration and capturing valuable data and tacit knowledge generated at the production facilities to support high-level decision-making towards reconfiguration. |
Table 2. GLN PLAST pilot line.
| GLN PLAST is a Mid Cap from Portugal, specialized in the mass production of plastic injection parts addressing very different markets such as automotive, consumer goods, medical devices, or food packaging. |
| Goal | Reconfigurable injection moulding cell for changing demand and material variations. |
| Production Process | Plastic part production via injection moulding. Plastic material is subjected to important fluctuation in price and availability. Moreover, because EU strategy on plastic usage and waste reduction, the use of recycled material reference is a new channel to foster in a resilient factory. |
| Main challenge | The specific challenges are the reconfiguration of the production according to customer demand, by considering the tooling step in order to adapt the CAPEX to the volume and the price of the part. Moreover, another challenge addressed is the reconfiguration of the production regarding material shortage and introduction of a new plastic material reference in the chain. |
| Vision | The reconfigurable concept is firstly based on the development of a Lego-like evolutive tool for injection molding that enables the plastic parts manufacturer to quickly test a market without purchasing large equipment such as molds. Moreover, by considering the material aspect of the supply chain of manufacturing, the demonstration will integrate the possibility to reconfigure the line according to material-related disruptions, such as quick changes of material references or integration of recycled material. |
Table 3. GESTAMP pilot line.
| GESTAMP is an international group dedicated to the design, development and manufacture of metal automotive components. |
| Goal | Reconfigurable laser-head to adapt to and optimise current production lines. |
| Production Process | The use case of GES considers design, development and manufacturing of suspension control arms for commercial vehicles. Key manufacturing processes for control arms are cutting, drilling, stamping and welding for local reinforcement. |
| Main challenge | Even for the same platform from a car manufacturer, individual components can have a variety of references depending on the car model or geographical market. These slight modifications require several changes in the production line, such as modifications of the manufacturing process/strategy, addition of small parts, or new tooling with a detrimental impact on downtime and manufacturing costs. In this context, flexible and reconfigurable production processes become crucial for a cost-effective adaptation of the production, providing the functionality and capacity required in the moment it is needed, while avoiding strict dependence to a single component reference. |
| Vision | Laser technology will be introduced as a solution for reinforcing specific variants of the control arms, avoiding necessity of many tooling to accommodate for different products, and thus enhancing the reconfigurability of the GES production. To identify this optimal configuration DT-based tools will be exploited to facilitate design space exploration. In addition, development and implementation of user interfaces with proper algorithms and protocols for reconfiguration control of the manufacturing process (workpiece setting up routines, process monitoring & control systems, safety chain) will be addressed for a cost-effective reconfiguration. |
Table 4. HALCOR pilot line.
| HALCOR is the copper and alloys extrusion division of ELVALHALCOR S.A. The current annual production capacity is around 90,000tn of copper tubes and the plant is the largest one in this sector in Europe. |
| Goal | Material rerouting algorithm to minimize scrap and optimize re-configurability in demand flux |
| Production Process | Cutting and selection copper tubing for various uses and markets |
| Main challenge | The key challenges faced by HALCOR is the high product mix in terms of quality requirements and product characteristics. Since QA results and other tube characteristics are not fully transferred horizontally within the production, there is a suboptimal allocation of semi-finished material to final products, limited capabilities for production reconfiguration, increased scrapped rate. In the case of coils, final quality focuses mainly on a number of potential defects per coil, as specified by the customer. Operators at the coiling phase do not have in advance the required knowledge on how many potential defects exist in the coming meters of the tube leading to scrapping several tube meters, when a coil exceeds, or it is estimated that it will exceed the limits set by the customer. |
| Vision | HALCOR wants to eliminate the manual transfer of information horizontally through the factory, as well as vertically to other production levels (engineering, management, etc.). This will enable to develop advanced (re) routing and (re) scheduling algorithms to optimize material flow within the production, reduce lead times and costs. These algorithms will merge with the existing Advanced Planning System that is used to assist in production scheduling. The part Digital Twin will enable full traceability and provide awareness to the successive production steps about the quality of the incoming material. Adaptive digital work instructions will be provided to coiling operators and will be constantly updated according to the digital signature of the tube that comes in the coiling station, thus enabling informed decision-making. |
Table 5. Gorenje Group pilot line.
| Gorenje Group is one of the leading European home appliance manufacturers with a history spanning more than 70 years. |
| Goal | Anticipating and adjusting tool wear to ensure production continuity |
| Production Process | Stamping of metal parts for kitchen appliances |
| Main challenge | Household appliances are subject to frequent design changes, since their design is fashion-driven to an extent, related to customer preferences in terms of interior design. Nevertheless, even minor design changes can lead to a significant disturbance of the production line and require several reconfigurations in terms of process and production planning, manufacturing strategies and fabrication of new tooling. A significant bottleneck in the reconfiguration workflow for GOR is the demand for redesign and remanufacturing of tooling (e.g stamping process dies) required during the reconfiguration phase, which can lead to several days of the production line being stopped |
| Vision | To introduce technologies to support the digitalization and reconfigurability of the production line of GOR, in order to eliminate disruptions in the production flow. Collaborative environments for co-development of the tooling will be introduced, to assess the impact of changes in the design, how it links back to the production and how modifications in design introduce needs for reconfiguration. ROMs (such as springback models) will also be developed, so that design changes can be quickly evaluated within the collaborative environment. Integration of supply chain awareness and quantification of supply chain disruptions on the tooling production line will be investigated to calculate sizes such as capacity and lead times and support the scheduling/planning algorithms of the whole production. |
Flex4Res.
In Flex4Res, four industrial use cases (see the short descriptions in
Table 6,
Table 7,
Table 8 and
Table 9) were selected for which project objectives were pertinent.
Table 6. Hans Berg pilot line.
| Hans Berg GmbH & Co. KG produces deep-drawn parts and metallic tubular components for the heating and automotive industry. |
| Goal | Reconfiguration measures after a tool change |
| Production Process | Adjustment measures are necessary when a tool or material has changed. Currently, it is performed manually, its duration and success depend on the experience of the employee executing it. Due to manual operation and several trials in adjustment, a high amount of material is turned into scrap |
| Main challenge | The adjustment measures are derived according to the defect pattern due to the absence of necessary information from inside the tool. The knowledge generated by an expert in reconfiguration and tool adjustment is tied to one product and can only be transferred to other products to a limited extent. |
| Vision | Integration of sensors inside machine tools enhance operational resilience by enabling real-time monitoring and data-driven decision making. The resilience assessment toolbox incorporating resilience measurement module measures machine resilience using historical and real-time data, and triggers reconfiguration as the resilience score descend. Reconfiguration toolbox comprises of fault detection and human assistance system. Human motion capture technology is employed that helps to identify and maintain knowledge database for corrective actions necessary for reconfiguration. By leveraging artificial intelligence, faults are detected early, and a decision support system suggests reconfiguration strategies accordingly. Operators are guided through human assistance system to ensure effective and accurate machine adjustments. Both the tools are offered as Software as a Service (SaaS) on Gaia-X compliant dataspaces. This will reduce the amount of produced defective components, the time required to reconfigure the tooling and the need for the experience required to perform the adjustment tasks. |
Table 7. Sidenor Group pilot line.
| Sidenor Group produces a variety of steel products (e.g., merchant bars, plates, wide rods and more) |
| Goal | Constant reconfiguration of supply plans |
| Production Process | Production processes range from scrap purchasing and metal processing to packaging and delivering to customers. |
| Main challenge | External and internal disruptions require reallocating the production to different production sites than originally planned. Currently, reconfiguration takes place manually and is based on expert knowledge and spreadsheet calculations. Moreover, decisions taken at the network level are not connected to the reconfiguration needed at the factory level |
| Vision | Based on a secure data exchange using IDS & Gaia-X connectors and the Asset Administration Shell (AAS) concept, the resilience assessment toolbox will guide the user through the steps for network reconfiguration by highlighting the differences with the current configuration status. In the production scheduler optimisation tool, an Artificial Intelligence (AI) agent will compute the scheduling of Thessaloniki’s plant based on the output of the Master Production Scheduling optimisation tool. The resulting schedule will be displayed to the user through a graphical user interface (GUI). |
Table 8. GOIMEK pilot line.
| GOIMEK is specialised in precision and large machining. |
| Goal | Production planning optimisation |
| Production Process | Their service begins with the preparation and treatment of high-performance materials, followed by advanced CNC machining including 5-axis milling and grinding, and concludes with strict quality control and final assembly to ensure precision and reliability. |
| Main challenge | All operations are performed in several working centres. The process steps are flexible but need to be fixed according to the daily production needs. Based on data from the ERP system a master production plan is generated, which is manually turned into a final production plan. Combined with a lack of flexibility these manual tasks cause inefficiencies reducing competitiveness as well as low predictability of production. |
| Vision | The production planner utilises real-time data from various sources to optimise the scheduling at the plant level proposing reconfiguration strategies and alternate schedules if deadlines are at risk. In addition, the predictive maintenance module will identify anomalies that could lead to failure. Since this will also impact production planning, actions will be suggested to enable a fast reconfiguration of the production to avoid unexpected problems. Moreover, secure data exchange based on the Gaia-X concept will be deployed to facilitate the communication between client and provider, using digital twins and the Asset Administration Shell (AAS). |
Table 9. Voestalpine group pilot line.
| Voestalpine group is a globally leading steel and technology group involved in the production and processing of high-performance materials |
| Goal | Reconfiguration of manufacturing processes during production |
| Production Process | Primary forming and alteration of material properties |
| Main challenge | The products required by customers vary in size and shape and can only be machined on machinery providing the necessary capabilities, which also vary on other factors such as tools. Therefore, highly flexible production planning and scheduling, also depending on the current machine state and manufacturing utilities, is needed. |
| Vision | A new shopfloor modelling approach will facilitate the integration of ERP- and machine capability as well as current configuration status data into a product, process, and resource model. Based on this a reconfiguration mechanism will be adopted, which allows a flexible flow of products through the factory. Errors will be detected through sensors and assessed through case-based reasoning. If necessary, measures for reconfiguration will be suggested. For disruptions coming from the supply chain, the resilience toolbox will allow the evaluation of missing capabilities and the need for reconfiguration. The resulting flexible and agile matrix production will enable the reconfiguration of the manufacturing process during production. |
Five pre-pilot cases were aimed to test and validate the resilience toolbox in different learning factory environments. Initially, various scenarios were developed to simulate production disruptions and test the effectiveness of the toolbox mechanisms. These scenarios were implemented in learning factories equipped with the necessary IT infrastructure. Learning factories have progressively expanded from local to international networks by testing different resilience strategies. Once the toolboxes are tested and fine-tuned, the services are ready for integration into industrial use cases. The pre-pilot cases were as follows.
•
PTW pre-pilot case: Create a generic pre-pilot case where some of the resilience and reconfiguration services are validated. This pre-pilot case is more generic, taking into account the requirements and specifications from all industrial use cases.
•
IFT pre-pilot case: The essential functionality of the Voestalpine use case was tested. The focus is on data flow, processing, and re-scheduling of manufacturing orders based on shop floor conditions.
•
LMS pre-pilot case: Set up the resilience assessment and reconfiguration strategy services of the Sidenor use case as well as the data space connectors and components. The goal is to validate the performance of the services early and to receive feedback from industrial experts.
•
IDEKO pre-pilot case: Test tools of the Goimek use case at the micro level, focused on (1) diagnosis cycles, (2) AAS Management, and (3) data spaces. The pre-pilot was set up at the Digital Grinding Innovation Hub (Ideko‘s facilities), where a Soraluce FMT milling machine was selected for testing.
•
USI pre-pilot case: Development and testing of tools for the Hans Berg case. Focusing on sensor integration inside machine tools to support operational resilience, designing mechanisms to measure machine resilience, and developing and testing reconfiguration tools at the resource level. Based on the resilience score, the goal is to trigger reconfiguration, detect reconfiguration needs early, and support machine operators to perform reconfiguration tasks effectively.
RaRe2.
In RaRe2, four industrial use cases (see the short descriptions in
Table 10,
Table 11,
Table 12 and
Table 13) and one value chain-oriented demonstrator were selected for which the project objectives are pertinent. These demonstration cases aim to evaluate performance in laboratory and operational environments, demonstrate rapid reconfigurability via the use of the tools, and gather feedback for continuous improvement. The industrial demonstration cases are as follows:
• MMM demonstration case: focus on validating and evaluating components for modular mobile sterilization units (RUMED). The goal is to simulate configurations to determine sensible, demand-oriented variants and check the completeness of the conversion and connection sets for rapid scaling in crisis regions.
• FONTANA demonstration case: To evaluate the performance of a single automated cell, a multiproduct line (MPL), for producing various car body parts. The focus is on using digital twins to simulate forming and assembly processes, optimizing costs and footprints, and managing daily peaks while ensuring zero-defect manufacturing.
• KARWALA demonstration case: Development of a process network and new data management systems to automatically identify and control subprocesses for producing child seats and face masks. The focus is on accelerating the development of urgently needed products and ensuring material availability by integrating recyclable databases into digital twins.
• MENICON demonstration case: Validation and evaluation of Digital Twin data architecture and BRIX platform extensions for prescription contact lens manufacturing. The goal is to test a predictive model of product quality based on physical data, creating a real-time feedback loop between the lens-lathing module and inline measurement systems.
Table 10. MMM pilot line.
| MMM is a European leader in the development and manufacturing of Reprocessing Units for Medical Devices (RUMED) with 65 years of experience. These units are one of the most important and sensitive areas of a hospital, providing the basic prerequisite for patients to be treated safely, quickly, and successfully. The professional reprocessing of medical devices is highly regulated and must follow a multitude of laws, guidelines, and various DIN, EN, and ISO standards. |
| Goal | Determine sensible, needs-based and rule-compliant configuration variants for mobile Reprocessing Units for Medical Devices (RUMED) to be deployed in crisis situations |
| Production Process | Reprocessing of medical devices and sterilizable products through sterilization, cleaning, disinfection, and endoscopy modules. |
| Main challenge | Rapid scaling of RUMEDs for deployment in crisis regions, dealing with the variability of sterilized goods, supply of media (water, electricity, gas), and adaptability to strict legal and certification constraints. |
| Vision | Double the baseline capacity (currently up to 28,000 units/year) through structural measures in module composition while complying with FDA and MDR aspects. Deliver a fully operational RUMED system within 4 days, reducing transport, assembly, and installation costs by 80%. |
Table 11. Fontana pilot line.
| Fontana Group is a leader in the luxury and sports car sector, renowned for its ability to shape aluminum with ambitious style lines. As the main partner of Ferrari for “body in white,” the group has a long-standing collaboration in creating the most challenging panels for the most renowned sports cars. The company is strongly export-oriented, with 95% of its turnover coming from exports of the finished product. Their comprehensive process chain covers everything from engineering, feasibility, and die manufacturing, to the stamping of class A full body panels and the complete assembly of “body in white” sub-assemblies
|
| Goal | Create a single automated cell, Multi Product Line (MPL), that produces many types of parts, allowing for high customization and rapid line reconfiguration |
| Production Process | Stamping of class A full body panels and assembly of complete “body in white” sub-assemblies using bonding, hemming, self-piercing, spot welding, and clinching processes. |
| Main challenge | Growing demand for more models with the same global production volumes, strict zero-defect manufacturing requests, shorter time to market, and the unpredictable assembly behavior of new “green” aluminum alloys that have variable mechanical properties. |
| Vision | Use digital twins to simulate forming and assembly processes, anticipate and compensate for defects before production, and optimize costs and footprint. Increase the average daily assembly cell capacity by 30% and reduce reconfiguration time by 2.7-fold |
Table 12. Karwala pilot line.
| Karwala is a European specialist in the production of child seats for cars, strollers, and various spare parts for such applications. One of their primary production methods is injection moulding, a process widely used across industries for the large-scale production of vehicle components due to its short process times and relatively low production costs. To ensure the highest level of safety, the child seats must be strictly categorized, tested, and approved in accordance with European Union regulations (such as ECE Regulation No. 44 or No. 129) |
| Goal | Develop a process network, new data interfaces, and new data management systems to automatically identify and control affected sub-processes, accelerating the development of new products |
| Production Process | Injection moulding for the large-scale production of vehicle components (such as child seats) and face masks. |
| Main challenge | Current individual process steps are mostly manual and not networked, preventing data transfer and processing along the chain. There is a need to accelerate development during sudden crises (e.g., pandemics) and ensure material availability by replacing virgin materials with recyclates on short notice. |
| Vision | Connect a digital twin with a material database for efficient simulation, automatically configuring recycled materials to achieve the exact same component properties while reusing existing mold inserts. The goal is to reduce FEM process time by 40% and the tool production process by 80%. |
Table 13. Menicon pilot line.
| Contact lens manufacturer Menicon serves the market for prescription contact lenses (PCL), which, unlike “regular” contact lenses made by cast moulding in large batch sizes, are customized and personalized to each individual patient. The lens design is based on specific measurements made by an optometrist and customized for every product. Due to this high degree of variability and complexity, the production of these customized contact lenses is a very labor-intensive process that requires the use of multiple specialized machines and many manual interventions. The heart of this process is the lathing of the lens from two sides (front and back). |
| Goal | Develop a fully automated and customized production line by creating a real-time feedback loop between the lens lathing module and an inline measurement system to ensure strict quality control. |
| Production Process | Customized lathing of the lens from two sides (front and back) based on an optometrist’s precise measurements for each individual patient. |
| Main challenge | Highly labor-intensive production, high costs, and highly specialized lathing machines that lack sensors and communication interfaces, making it impossible to monitor and adjust process parameters in real time. |
| Vision | Double the production capacity to 3,000 lenses per day, significantly reduce human errors (dropping the rejection rate from 15% to 1–2%), and decrease production costs by 70% per lens by utilizing digital twins to generate machine parameters and correlate quality measurements |
Identifying and mapping risks and disturbances in various industries
If we look at the first steps in increasing resilience capability, we start by the need to understand the type of disturbance or risk that a company or sector is facing and the severity of that risk to a disturbance or actual disturbance taking place (see
Figure 3). The need for industries is clear, as a recent (2021) WEF report states that, using a resilience self-assessment method, according to this method only 12 percent of companies can be called resilient. Based on two recent HEU-funded projects dealing with improving resilience among EU manufacturing industries and drawing from the literature, we discern various levels on which resilience can be improved in practice. Companies can take measures at the supply chain, factory, resource, or device level.
Figure 3. First steps in increasing resilience capability.
When examining several pilot lines developed in the two projects introduced above, based on interviews and company-as well as sector-wide indicators, we attempted to identify the key disturbances and risks identified by these companies that could serve as a trigger to start a resilience strategy, such as reconfiguring a production line. In the examples below, we provide the first evidence from different industries trying to increase resilience. In pathways towards increased resilience for EU industries, there are several steps to be taken, including gathering and understanding different types of risks of disturbances per sector or economic activity, understanding the level, and thereby the role of digitization in resilience strategies, and establishing a baseline of reconfigurability, one of the resilience strategies we are focusing on, as well as applying useful metrics on progress both in reconfigurability and resilience. The two projects apply a slightly different scope when it comes to resilience strategies and tools to capture disturbances and mitigate risks. The Flex4Res projects take the perspective of macro, meso, and micro, where macro refers to the supply chain, meso refers to the production system level, and micro refers to machinery or device level, whereas the R3group and RaRe2 projects look at the factory level, system level, and workstation level. In all projects, these classifications were used to describe the target area of a project solution or outcome. The common point is that the projects aim to connect levels of disturbances or risks to a variety of possible technical responses (this can be a tool, a method, or a computer program) that we propose and are currently developing in our respective projects[5]. Looking into several industry examples via different steps, we start with the types of disturbances and risks[6] described above, and look at different risk categories, divide them into a scale, and where possible, a likelihood and severity (linked to the JRCs disturbance indicators of severity and duration of exposure). These scores were based on interviews with the company in question and desk research on the typical risks or disturbances for the sector in which the company is active. In the examples below, we have different-sized companies that are active in different domains.
In the Flex4Res and R3group, some forms of scales have been used in interviews and surveys with pilots to indicate risks or disturbances, their likelihood of occurrence, and the severity of such a risk or disturbance. The following scales were provided (see
Table 14 and
Table 15):
Table 14. Severity scale.
| Severity [1–5] | Title | Description |
|---|
| 1 | Insignificant | No significant consequences |
| 2 | Minor | Some inconvenience but no serious damage |
| 3 | Moderate | Disruption or damage manageable with effort |
| 4 | Severe | Significant damage or disruption that needs immediate intervention |
| 5 | Catastrophic | Complete failure or critical damage with long-term consequences |
Table 15. Risk scale.
| Risk [1–5] | Title | Description |
|---|
| 1 | Negligible | Insignificant risk; minimal impact on objectives |
| 2 | Low | Minor risk; unlikely to affect objectives significantly |
| 3 | Moderate | Manageable impact but needs attention |
| 4 | High | Could cause considerable impact if not mitigated |
| 5 | Critical | Severe impact on objectives and requires immediate action |
From the
Table 16, we can see that all the companies in the two projects display a variety of risks or disturbances that range from the macrolevel (production network) to the microlevel (machine or device level). Some of the disturbances mentioned have to do with external factors that can have an impact beyond one company production line, such as rising energy costs, geopolitical instability, and market disruptions, whereas others are due to internal production line factors. Here, we can see examples of workforce, skills, and the lifetime of machines or tools as disruption factors. In both projects, the abovementioned disturbances can be roughly categorized as sector-wide and often intra-national disruptions in the supply chain and/or global prices of either raw materials or energy, disturbances that take place at the factory level, and challenges of maintaining stable production levels in the context of volatile demands or factory-asset breakdown as well as scheduling problems. While the former is at the heart of the topic of resilience, the latter can be equally seen as a resilience challenge, specifically in the context of European manufacturing, where it is of key interest to prolong the life of tooling and machinery, and where the workforce in manufacturing is ageing.
Table 16. R3GROUP & Flex4Res disruption likelihood.
| Pilot line company | Hierarchical level | Disruption | Level | Likelihood | Severity |
|---|
| Sidenor | Macro | Raw material fluctuation | Critical | 4 | 5 |
| Changes to the energy cost | High | 4 | 4 |
| Changes to transportation costs | Moderate | 4 | 2 |
| Meso | New orders arrival | Moderate | 3 | 4 |
| Meso | Resources breakdown | High | 4 | 4 |
| Meso | Raw material issues (unavailability, quality) | Moderate | 3 | 4 |
| Voestalpine | Meso | Task (or job) failure | High | 3 | 3 |
| Goimek, Voestalpine | Meso | Anomalies in machining process | High | 3 | 4 |
| PTW pre- pilot case | Meso | Equipment (or labor) failure | High | 3 | 4 |
| Hans Berg | Micro | Components failure | High | 4 | 5 |
| Maintenance | Moderate | 3 | 3 |
| Katty Fashion | Micro | Operator unavailability | Extremely high | 4 | 4 |
| Macro | Volatile demand | High | 3 | 4 |
| Macro | Market changes | Medium | 4 | 2 |
| GLN plast | Meso | Batch size or order quantity policy | High | 4 | 3 |
| Macro | Sudden hike in costs | High | 4 | 3 |
| Gestamp | Macro | Volatility in automobile part demand due to geopolitical instability | High | 5 | 4 |
| Meso | Rising energy costs for laser welding | High | 4 | 3 |
| Halcor | Macro | Volatility in copper markets and supply | High | 3 | 4 |
| Meso/Micro | Loss of material due to suboptimal use of production line and quality control | High | 4 | 3 |
| Gorenje | Micro | Sudden stamping tool breakdown | High | 3 | 5 |
In discussions with different pilot lines, and the reasons they participate in research and innovation projects like these ones, many mention, most logically, the covid-19 pandemic and geopolitical turmoil as core external disturbances for production, with energy prices, supply chains, and changing demands affecting day-to-day operations. Regulations are rarely mentioned as a source of disruption, or at least not in the short term. One of the recurring themes among these companies is information sharing, planning, and accessibility. Digitization of SMEs, as it turns out, has not gone as far as perhaps hoped, with digital integration at the company level being only at the early stages in many of our pilot line examples. A striking yet perhaps obvious point is that many departments within SMEs still work in digital silos, with elements such as company strategy, goals, planning or budgets often not clearly communicated or accessible. In addition, a myriad of tools and portals for both administrative and substantive tasks are often used in parallel, with a clear data-as-company-asset strategy or missing plan. However, a clear digital strategy and roadmap are precursors for increasing resilience and reconfigurability capacity building.
In the section below, we delve into different anticipation and response strategies to external disturbances and the technological tools we are developing in projects that aim to increase resiliency among these companies and, ideally, the wider sector they are a part of.
Tools to address resilience and reconfiguration
Once a risk or disturbance has been identified and marked as significant to such an extent that it can lead to disruptions in production, the next step is to find the correct response (see
Figure 4). This response should fall within the boundaries of what a company is able to do or is in control of, or the levers it is able to pull. The previously mentioned resilience capabilities compass and other frameworks can prove informative in establishing a way for companies to self-assess their level of resilience vis-à-vis a particular kind of disturbance. Much in line with the Digital Maturity Assessment tool that exists for SMEs[7], there is a need for assistant in resilience-self assessment which can guide companies to develop better strategies and make more targeted investments in shopfloor equipment and personnel training, to name a few.
Figure 4. The next step - to find the correct response.
In the three projects considered, we are developing tools that address resilience challenges on different levels (macro, meso, and micro) and that all have a digital core or component (see
Table 17). In these projects, reconfigurability plays the role of resilience strategy or response. We briefly highlight some of these tools at each level and discuss resilience and reconfigurability tools in detail, one at each level. After this section, we will discuss the strategies and challenges for increasing resilience in manufacturing.
Table 17. Examples of different tools to increase resilience and reconfigurability capabilities.
| Project | Macro | Meso | Micro | Responds to Core trigger | Sector |
|---|
| Resilience
| Flex4Res | Resilience assessment – Supply chain | | | Changes to the raw material prices, changes to the transportation costs | Metal sector |
| Flex4Res | | Resilience assessment –Shopfloor value stream | | Equipment (or labor) failure | Metal sector |
| Flex4Res | | | Resilience assessment –Resource | Resource breakdown | Metal sector |
| R3Group | Supply chain risk modelling | | | Before a trigger – the tool is the basis for reconfigurability triggers | Several (metal, textile, plastics, copper) |
| R3Group | | Weak signals analysis | | Before a trigger – the tool is the basis for reconfigurability triggers | Several (metal, textile, plastics, alu welding) |
| RaRe2 | Early detection
reconfiguration need tool | | Before a trigger – continuous external-signal monitoring and early warning for reconfigurability needs | Several (metal, textile, plastics, copper, welding) |
| RaRe2 | | Skill gap detection tool | | Before a trigger – the tool is the basis for reconfigurability triggers | Universal |
| RaRe2 | Matchmaking tool to search partners | | | Before a trigger – the tool is the basis for reconfigurability triggers | Universal |
| Reconfigurability
| Project
| Macro
| Meso
| Micro
| Responds to Core trigger
| Sector
|
| Flex4Res | Master Production Scheduler | | | Planner trigger tool to compute new plan | Metal sector |
| Flex4Res | | Productions scheduling tool | | Planner trigger tool to compute new plan | Metal sector |
| Flex4Res | | | Fault detection and human assistance system | Trigger and support worker to perform reconfiguration | Metal sector |
| R3Group | | Virtual Collaborative Environment for quick redesign | | Triggered by design and planning/production outlook | Textile sector, plastics sector |
| R3Group | | Productions scheduling tool to minimise scrap | | Triggered by production planner | Copper tubing sector |
| R3Group | | | Automatic mold insert replacement to adapt to new demand or material change | Triggered by task programmer/operator | Injection moulding sector |
| RaRe2 | | Production Optimization tool | | Triggered by production planner | Contact lens production |
| RaRe2 | | | Multi Modal Guidance System | Triggered by operator | Car body parts production, metal sector |
Deep dive macro/meso tool (RaRe2 – Early Detection Tool)
Production process.
Across pilot lines, external disturbances such as raw-material shortages, transport disruptions, energy price spikes, geopolitical events, and changing regulations can lead to late deliveries, demand shifts, or sudden cost increases. Currently, the detection of such risks is often based on ad hoc monitoring by individual experts or on lagging indicators, which means that disruptions are only recognised once they have already materialized in the production system (e.g., delayed orders, missing materials, abrupt re-scheduling).
Resilience– and reconfigurability challenge.
The key challenge is to strengthen awareness and anticipation at the macro and meso levels: SMEs and mid-caps need a systematic way to detect weak signals of external shocks early enough to prepare reconfiguration scenarios, but they lack dedicated risk-intelligence teams and task-specific AI models. Relevant information is scattered across unstructured sources (news, policy documents, supplier announcements, and market reports) and cannot be easily linked to company-specific supply chains, contracts, and production constraints. As a result, reconfiguration actions (e.g., alternative routings, tooling strategies, and sourcing changes) are often reactive rather than proactive.
Proposed solution.
The Early Detection Tool, developed in RaRe2 and integrated into the RaRe2 Holistic Tool Ecosystem, was based on locally operated Generative Pretrained Transformer (GPT) models.22 It combines two types of inputs (see also
Figure 5):
• public data, such as news articles, macroeconomic and market indicators, regulatory/legal texts, and
• internal context, such as a structured supply chain profile (tiers, geographies, critical materials, lead-time sensitivities) and relevant documents (contracts, supplier information, OEM requirements).
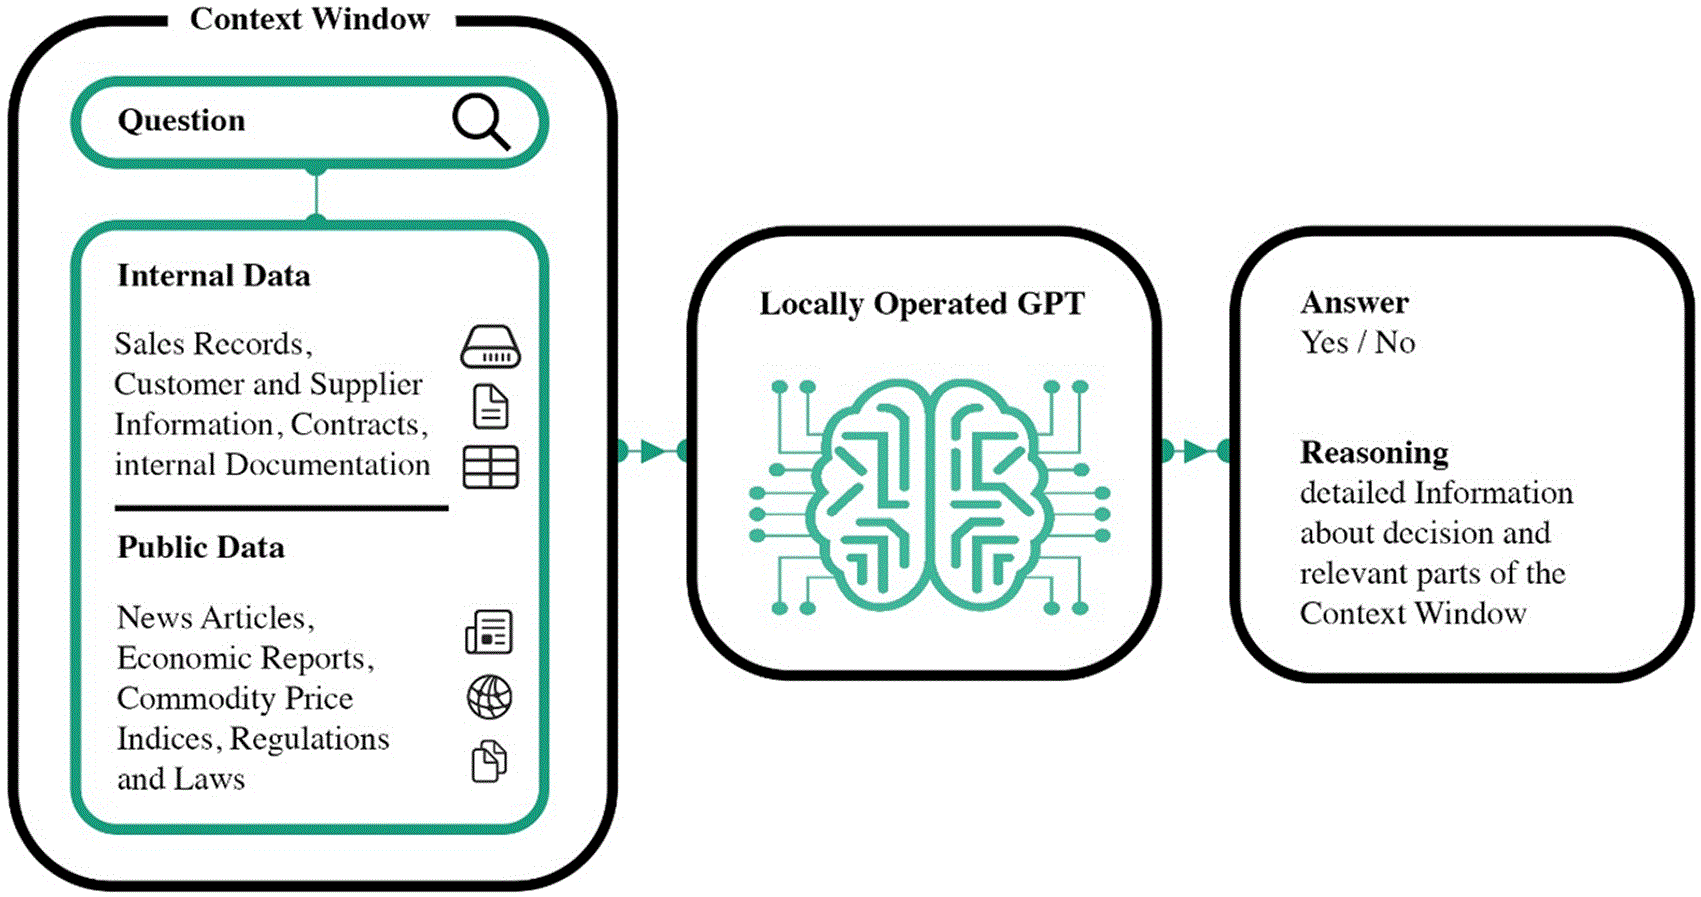
Figure 5. The system integrates external data sources (news, economic indicators, regulatory documents) and internal company context (supply-chain profiles, contracts, supplier information) through a locally operated Generative Pretrained Transformer (GPT) model using zero−/few-shot learning.
The tool generates structured outputs—an answer and explanatory rationale—enabling decision-makers to anticipate disruptions and prepare proactive reconfiguration scenarios before they materialize in the production system.
By exploiting zero−/few-shot capabilities of GPT models, the tool operates without task-specific training data. It uses the model’s context window to merge company profiles with selected external documents and returns structured outputs: an early-warning/risk score (0–10) and a short textual rationale that can be reviewed by human decision makers.23 A full prototype pipeline crawls news (e.g., via news-please), runs local GPT inference (Llama-3.1-class models), and generates JSON-structured results that can be consumed by other tools in the resilience toolbox.
The empirical evaluation of an augmented, labelled dataset (~30 k articles across 36 scenarios and 195 countries) shows that the system can moderately distinguish events that affect or do not affect a given supply chain, despite strict binary labels and no task-specific training. On historical unlabeled news (~42 k articles from 78 outlets in 13 languages), the tool reliably flags major shocks (e.g., natural disasters, conflict escalation) as a high risk for relevant supply routes. Behavior is deliberately conservative (some false positives), which is acceptable for triage and decision support rather than autonomous control.
Impact for the company.
The Early Detection Tool acts as a macro/meso-level “front-end” service rather than a planning or control tool. Its early warnings and explanations are as follows:
• trigger scenario runs in supply chain digital twins (e.g., for Katty Fashion) and in macro-level resilience assessment tools based on penalty-of-change (PoC),
• inform master production scheduling and plant-level production scheduling of likely upstream disruptions (e.g., material shortages, logistics bottlenecks, regulatory changes), and
• give shop-floor stakeholders additional time to prepare reconfiguration actions (e.g., alternative routings, modular tooling strategies, buffer stock decisions).
For SMEs, the local deployment of GPT models addresses confidentiality concerns while avoiding the need for large labelled datasets. The tool thus increases awareness and anticipation without imposing heavy data science requirements on individual companies, and strengthens the overall effectiveness of the reconfiguration toolbox by ensuring that downstream tools are triggered early enough to have an impact.
Deep dive macro tool (Flex4Res)
Production process.
One pilot line concerns a steel manufacturing group that produces a large variety of steel products such as wire rod coils, rebar coils, and straight rebars, which are used in multiple industrial sectors. Specifically, the facilities within the steel manufacturing group include enterprise-level operations, warehouses, and manufacturing plants, which are all integral components of their steel production infrastructure. Furthermore, the steel manufacturing group spanned nine facilities across four countries. The presence of uncertainties and disruptions in the operating environment poses significant risks to the execution of a supply chain plan of six or twelve months, potentially leading to deviations from planned schedules, increased costs, and compromised fulfilment of customer requirements.
Resilience– and reconfigurability challenge.
A Master Production Scheduler (MPS) is a reconfiguration strategy service that aims to compute a supply chain plan. The tool deals with planning the production, storage, and transportation of certain commodities in a profitable and effective manner for the organization. By forecasting market demand for a decision horizon of one or five years, MPS aligns production and operation planning with demand fluctuations, helping manufacturers optimize resource allocation and adjust to disruptions. Owing to the fact that forecasting the market demands, raw material prices, energy costs, etc. is difficult to achieve accurately for a decision horizon of one or five years, there is a need to proactively assess how resilient the manufacturing system is and the plan that is selected for industrial planners. The goal of the resilience assessment service for the supply chain is to evaluate the behavior of the supply chain system under unexpected circumstances before the application of a supply plan.24
Proposed solution.
To assess the resilience of the supply chain system or plan, the Penalty of Change (PoC) methodology is used to estimate how a system will be affected by potential external or internal changes, such as machine malfunctions or market shifts (see also
Figure 6). The expected cost of these changes is calculated by multiplying the penalty (cost) of each scenario by its probability of occurrence.25 This method requires defining the scenarios, their probabilities, a predefined objective function, and penalties. The final result was the sum of all penalties adjusted by the likelihood of each scenario, offering an assessment of the system’s resilience. The resilient assessment approach is used to assess different supply chain plans with the same input, but applying different business constraints (e.g., scrap plan, demand, plan, operational models for the facilities, etc.), and to support industrial planners in selecting the most resilient plan that maximizes the overall profitability of the production network.
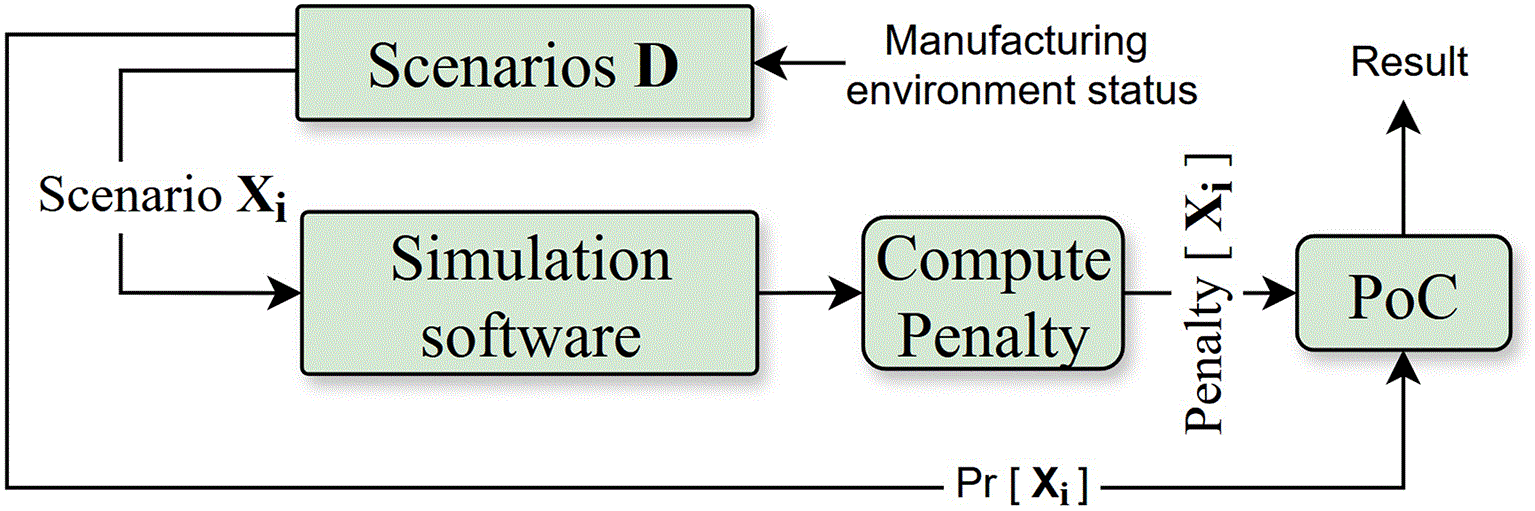
Figure 6. Resilience assessment approach utilizing the Penalty of Change (PoC) methodology: Macro level.
Impact for the company.
Based on workshops with industrial experts, the expected benefits of implementing a resilience assessment service for the supply chain aim to improve a) the overall profitability of the network through optimized production processes, b) enhanced resource utilization, and c) reduced operational costs.
Deep dive meso tool (Flex4Res)
Production process.
The production process in the steel manufacturing group involves various stages (see the deep dive macro tool), from raw material procurement to the final production of steel products. However, disruptions, such as unplanned machinery breakdowns, unexpected orders, or raw material shortages, can lead to significant production delays and deviations from the planned schedule. These disruptions complicate short- and mid-term planning (weekly or daily).
Resilience – and reconfigurability challenge.
The primary challenge is the need to quickly adapt to unforeseen disruptions such as machinery breakdowns or sudden changes in customer orders, which can vary in terms of complexity and urgency. These disruptions can lead to shifts in production priorities, requiring the fast reconfiguration of resources and production schedules to minimize downtime and meet customer demands. The ability to maintain continuous production and optimize resource utilization under these conditions is a key challenge. To overcome these challenges, it is essential to integrate advanced resilience mechanisms and adaptive scheduling systems that enable plants to respond swiftly and efficiently, minimizing the impact of disruptions on overall production performance.
Proposed solution.
The proposed solution to address the resilience and reconfigurability challenges involves a Production Scheduling tool to compute the production schedule (see
Figure 7). Through the PoC methodology, this tool proactively simulates production disruptions and evaluates the impact of reconfiguring production schedules. By leveraging a digital twin implemented with Asset Administration Shell technology, the tool ensures quick adaptation to unexpected events such as new orders or machinery breakdowns. It enables dynamic re-scheduling and effective resource reallocation, maintaining operational continuity, and optimizing production efficiency.
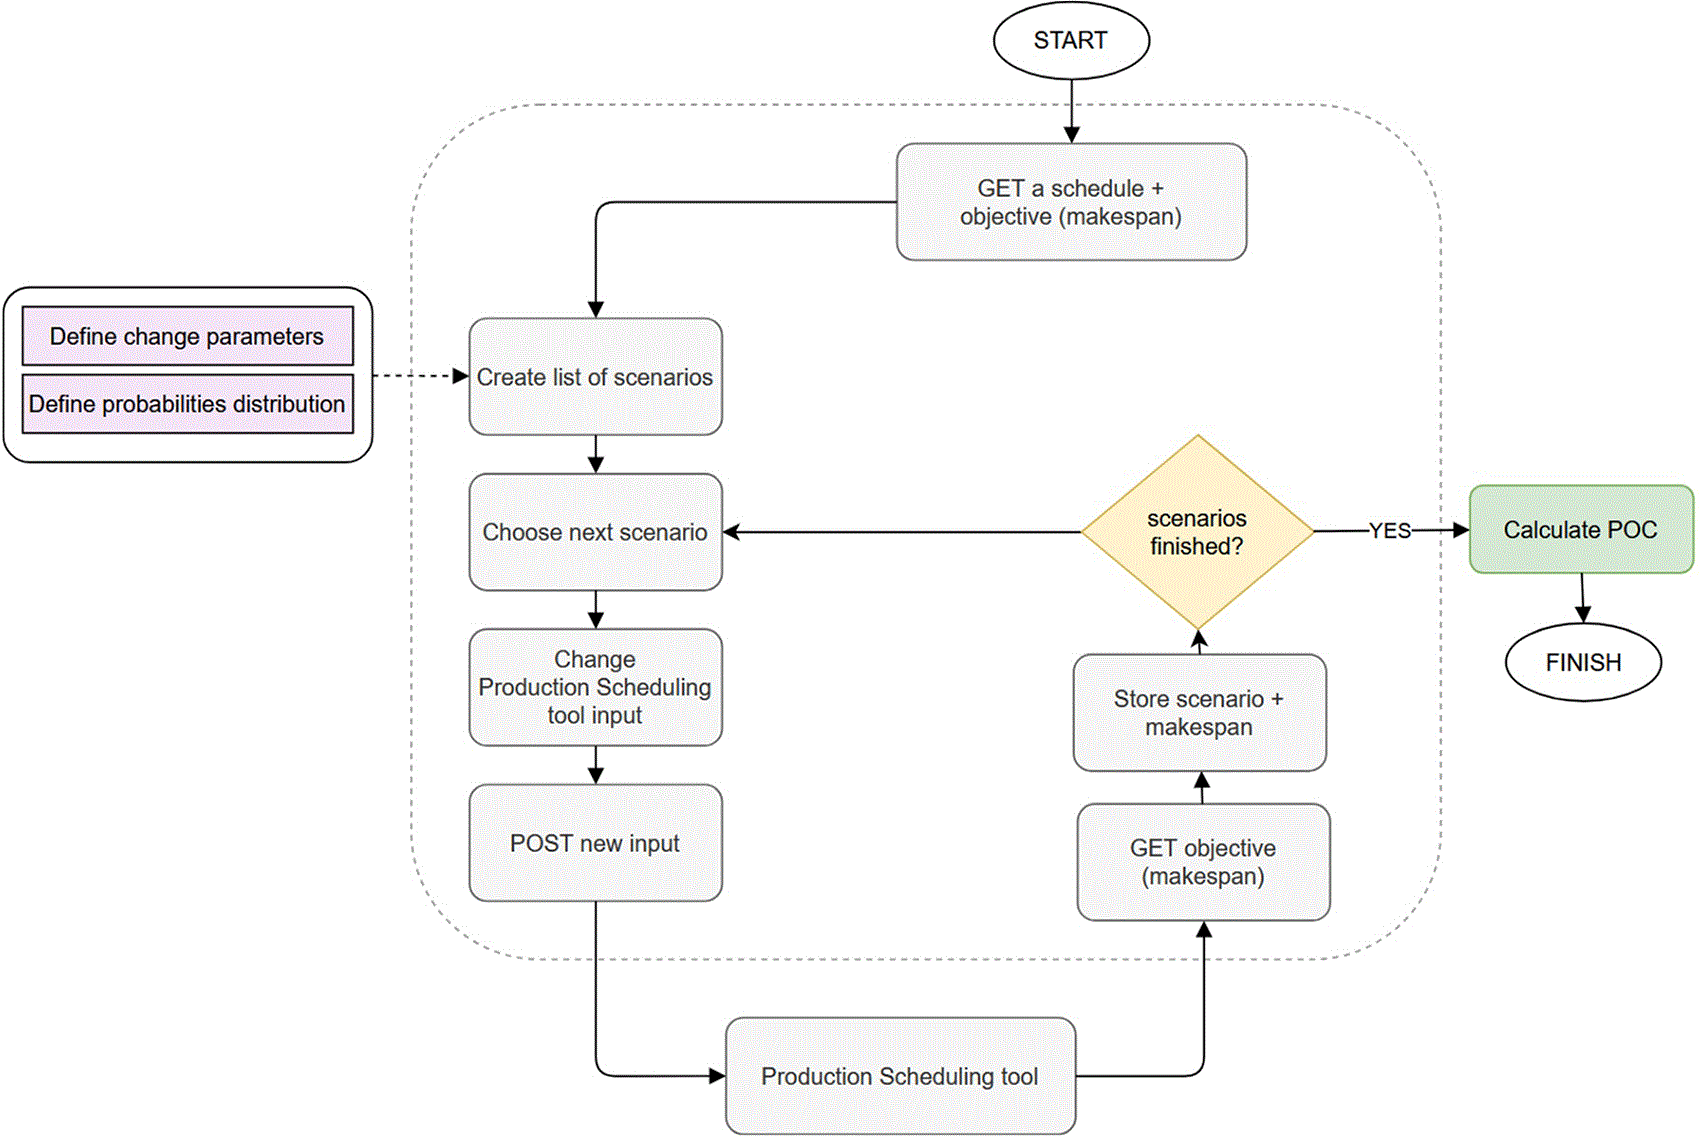
Figure 7. Resilience assessment approach utilizing the Penalty of Change (PoC) methodology: Meso level.
Impact for the company.
Based on workshops with industrial experts from the plants of the group, the expected benefits of implementing the resilience assessment service for the production system aim to improve a) minimize production downtime, b) enhance resource utilization, and c) reduce reconfiguration time.
Deep dive meso tool (R3group)
Production process.
Focusing on the supply chain aspect of this pilot line (see
Figure 8), Katty Fashion’s supply chain includes multi-tier suppliers, with materials coming from different parts of Europe (mainly Italy and France). These materials are transported by road or air, depending on the customer delivery requirements. Once production is complete, finished garments are distributed to client distribution centers across Europe.

Figure 8. Typical production steps in textile manufacturing.
Resilience– and reconfigurability challenge.
A company in the textile and garment manufacturing sector, Katty Fashion, deals with high supply chain volatility, and disruptions can have major effects on production lines and capacity. They operate in a highly competitive environment influenced by evolving regulations and demand volatility. The company faces limited visibility beyond first-tier suppliers, making risk-mitigation strategies crucial. Additionally, Katty Fashion has no flexibility in supplier selection, as materials must be sourced from suppliers chosen by the client or the OEM. This constraint reduces the agility in managing supply disruptions. Such disruptions can significantly affect the end-to-end order lifecycle. In relation to supply chain risks, the main resilience challenges are
• Market and demand volatility: Rapid shifts in consumer preferences and regulatory changes require early detection and proactive adaptation.
• Employee Unavailability: Labour shortages can disrupt production schedules and reduce operational efficiency.
Proposed solution.
One of the tools developed for this pilot line is the Supply Chain Digital Twin (SCDT). In this Digital Twin, the prices and sources of raw materials are tracked, and both in-company and external data are used to train and test different models in relation to several scenarios (business as usual, do-nothing scenario with demand variation, and do-nothing scenario with material shortages). Moreover, DT covers different scenarios related to personnel shortages and/or falls and the costs of finding and retraining or upskilling current or new personnel. Below (
Figure 9) is an impression of some of the first SCDT results showing the impact of the change in demand on resource scheduling:
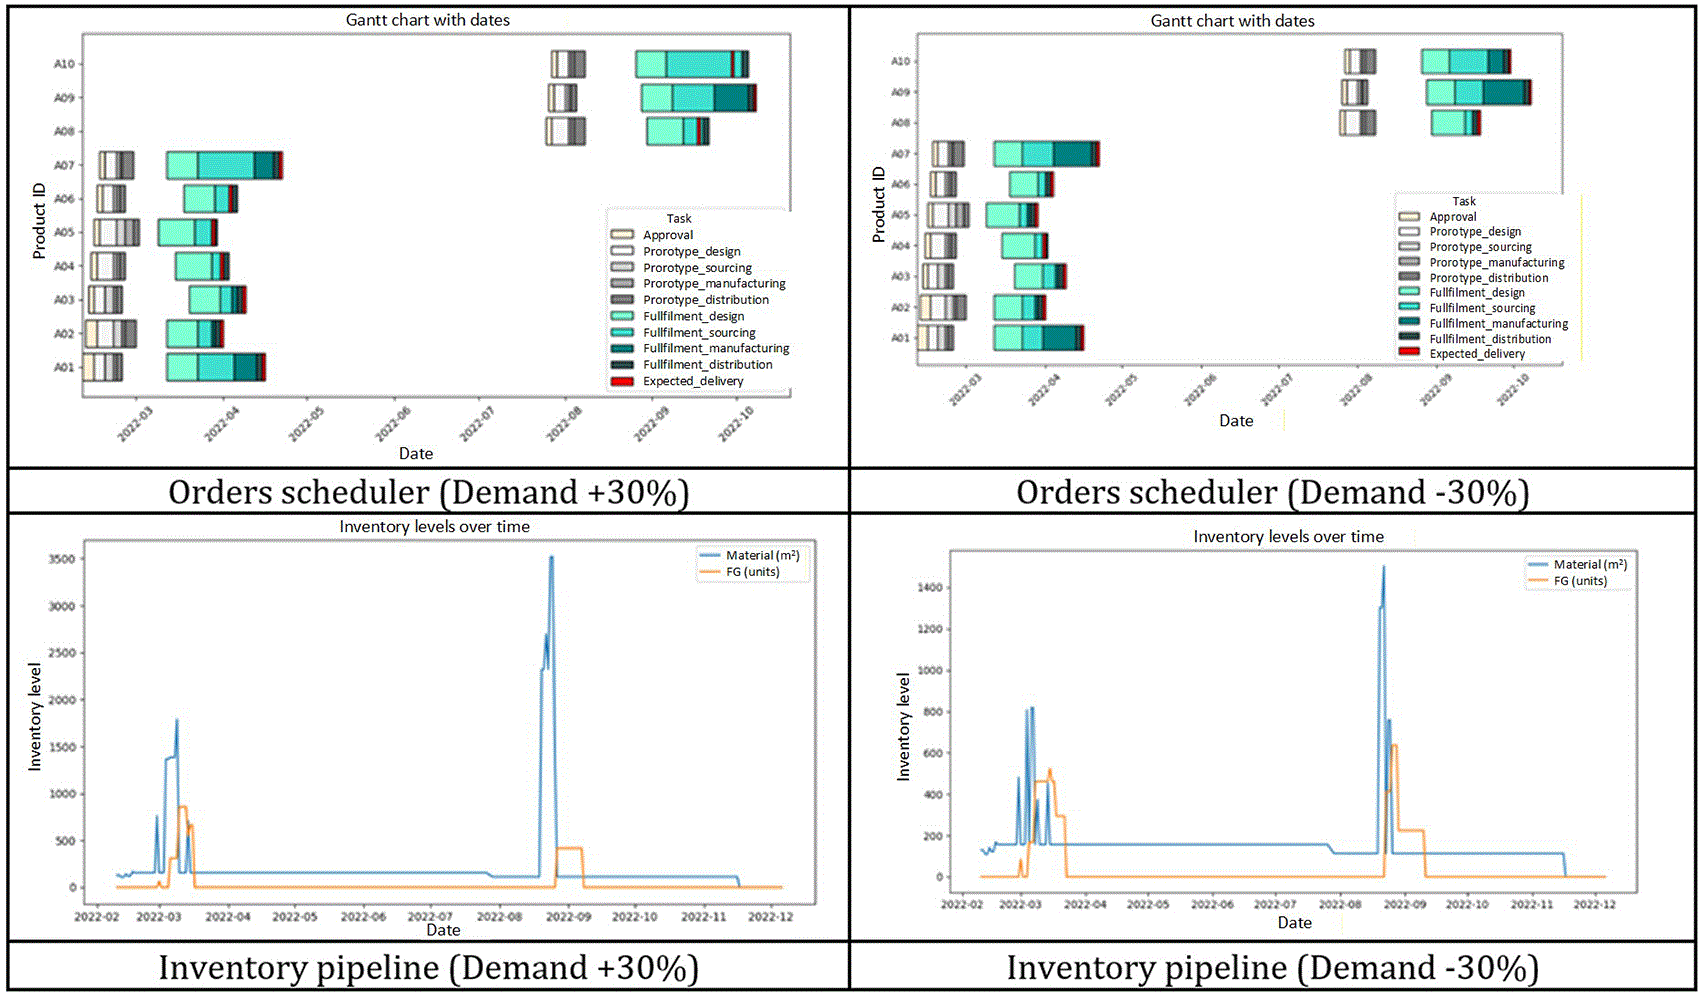
Figure 9. DT prediction for different disruption scenarios for textiles.
Impact for the company.
As for the material and demand DT, we can see that a 30% demand increase compresses production schedules, creating potential bottlenecks, while inventory levels spike due to frequent replenishments. In contrast, a 30% drop in demand leads to more relaxed scheduling, reducing operational strain but increasing resource underutilization. Inventory remains stable, minimizing supply chain pressure but risking inefficiencies. The Gantt chart reflects extended cycle times, allowing for more flexibility. By integrating optimization models, the company can enhance both resilience and reconfigurability, and dynamically adjust operations to maintain efficiency and adaptability across varying demand scenarios. As for Personnel DT, the model enhances the company’s resilience and reconfigurability by improving its absorptive, flexible, and transformation capacities. Training programs ensure that employees can adapt to new machinery, while hiring and managing part-time workers offer flexible staffing approaches that improve adaptability, and labor forecasting supports long-term strategic planning.
Deep dive micro tool (R3group)
Production process.
In the case of GLN Plast, the production process we focus on is injection molding. By serving many different OEMs, GLN produces parts that are complex in geometry and high in volume. Both the chosen material and the quality level sought after were set by the external client.
Resilience– and reconfigurability challenge.
For GLN, the challenges related to resilience are connected to the ability to adapt to market demand changes, which are slight changes or adjustments needed for a product, as well as fluctuations in material availability and quality due to geopolitical developments and regulations in relation to the update of recycled material in their production lines. In terms of reconfigurability, one of the challenges with injection molding is the time and costs of mold development and the relatively low level of digitization of injection molding machines to other parts of the production process, such as quality inspection. While the injection molding process is extremely effective for the mass production of low-cost, high-quality plastic products, the mold itself is a significant bottleneck for reconfigurability. Even the slightest design change of the final product requires the redesign and remanufacturing of the mold cavity, leading to significant capital expenditure and a lack of reactivity to market demand.
Proposed solution.
To facilitate the reconfigurability of plastic forming processes, we have developed an approach for modular molds for rapid reconfigurability, owing to interchangeable mold inserts and standardized interfaces for insert clamping and cooling that enable fast mold cavity exchange. Although interchangeable mold inserts already exist commercially, the solution developed is to digitally connect all the steps in the process, from material characterization to quality prediction, process monitoring, and quality control, and to automate as many steps as possible in the reconfiguration process. Below (
Figure 10) is an image showing the virtual setup of the reconfigurable injection molding cell and the digital thread architecture of the cell.
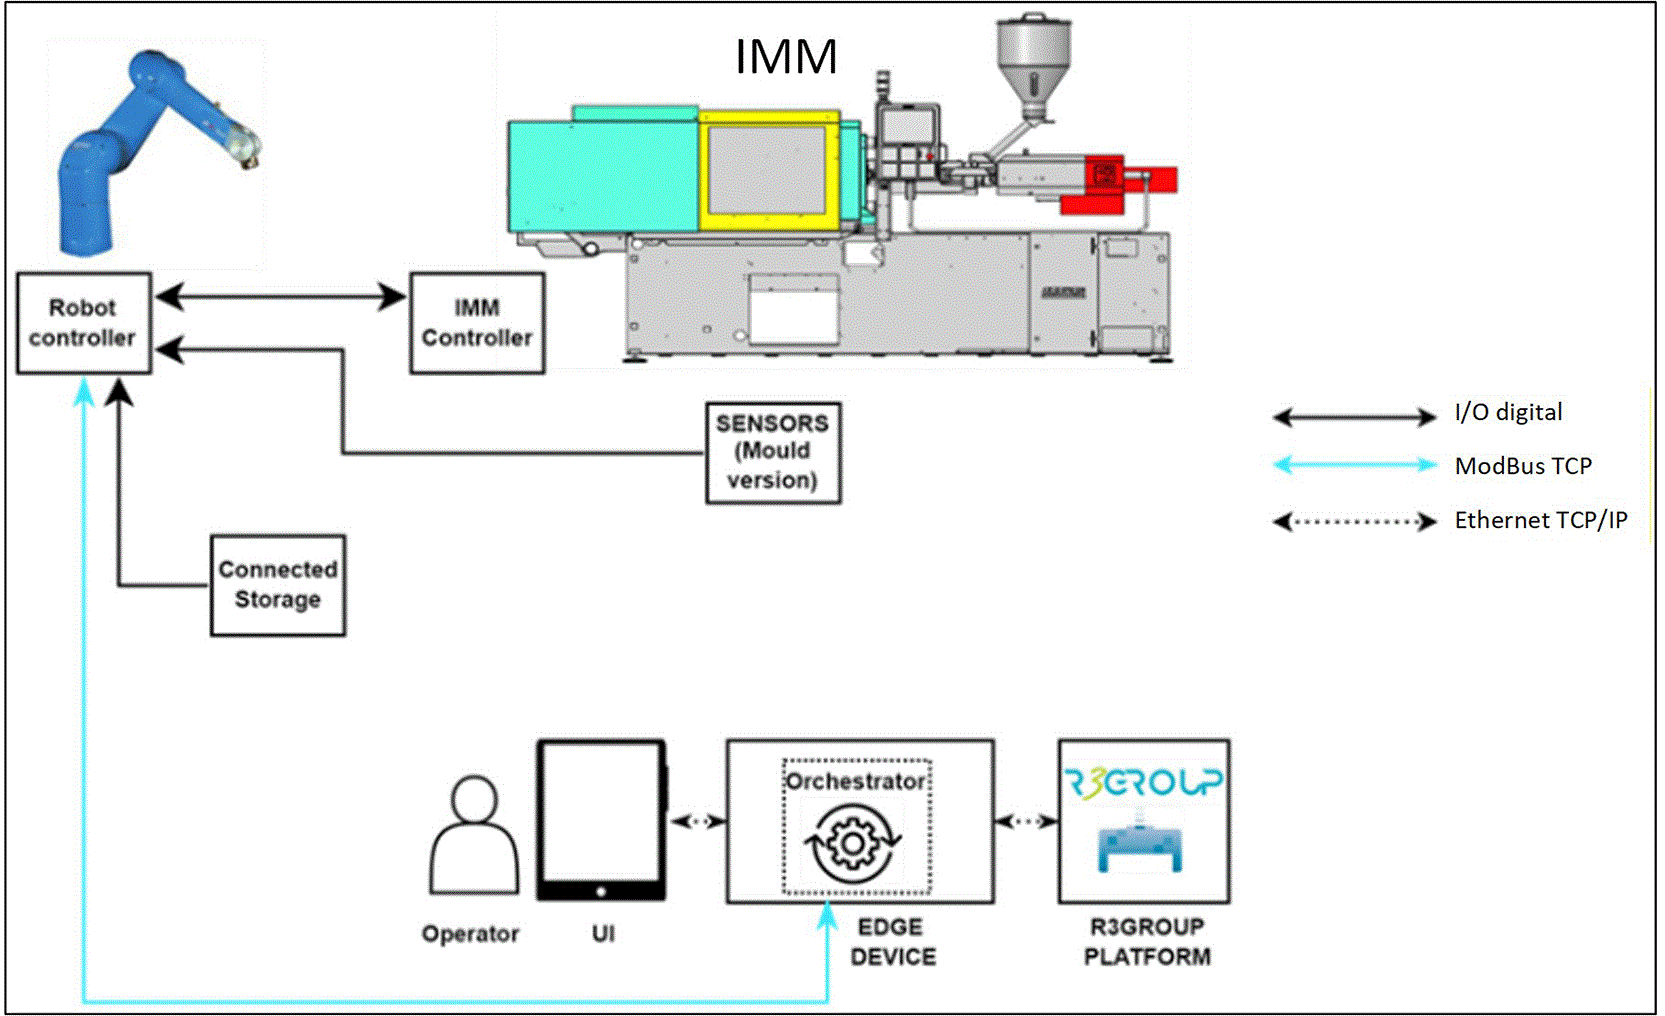
Figure 10. Simplified schedule of injection machine automation for reconfiguration.
Impact for the company.
As for the product chosen for the pilot, among the 285 commercial references produced by GLNP, 4 parts of interest for R3GROUP have been selected. All the proposed parts are available in several versions. Below (
Figure 11) is the design of the different changeable in-mold inserts and the tested mold with the two product variants. The product has two versions, A and B, which can be produced with the reconfigurable injection molding cell by changing the inserts in the mold.
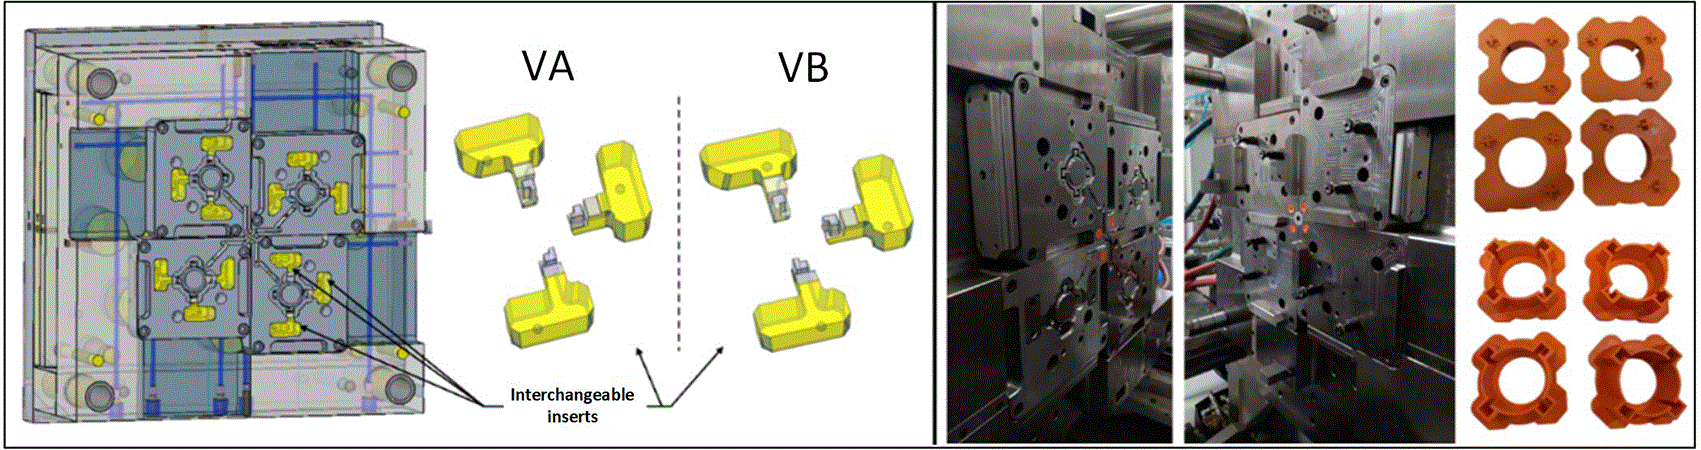
Figure 11. Different mould inserts ensure quick versioning of products within the same product family.
To evaluate the relevance of the solution adopted by GLNP, a comparison with conventional solutions was made by examining the initial market condition followed by market changes. For each situation, the impacts on CapEx, process cost per part, production reconfiguration time, and reactivity to market evolution (tool manufacturing lead time) were calculated. By comparing three different manufacturing solutions to the challenge of dealing with different versions of a product with different market scenarios, an economic assessment was performed on the viability of our reconfigurability solution. In 3 following scenarios, we looked at the consequences for the capex of our solution:
• A major change in the market occurred, and the need for version A dropped to 25%, while the need for version B increased to 75%.
• Introduction of an additional version C, which is a combination of versions A and B. A new volume mix is now established at 25% A, 25% B, and 50% of C.
• The regulations applicable to this product are modified in some countries, leading to the introduction of an additional version, D. The new volume ratios were set to 20% for A, 20% for B, 20% for C, and 40% for D.
In this example, we can see that rapid reconfigurability, while perhaps needing an initial higher capex, over time could become attractive both in terms of costs and time needed to adjust the production line to new demands.
Resilience and reconfigurability strategies
Resilience in manufacturing and supply chain systems is critical to ensure that operations can withstand disruptions and maintain continuity. Resilience (see
Figure 12) can be increased in two ways: 1) by making plans (such as sales and operations plans, production plans, and production schedules) more robust, or 2) by enhancing the environment’s ability to respond to and recover from disruptions. These approaches can be categorized into proactive and reactive strategies, each of which contributes to a more resilient system.
Figure 12. Increase of resilience capability.
Making resilience plans more robust
Building a robust resilience plan for manufacturing involves both proactive and reactive strategies that work together to ensure that systems can withstand and recover from disruptions effectively. Resilience is built by identifying potential risks, such as supply chain disruptions or machinery failures, and preparing for them. Predictive analytics powered by AI can anticipate problems such as equipment breakdowns, enabling preventive maintenance, or adjustments to production schedules. Additionally, integrating flexibility into planning, such as diversifying suppliers and adopting adaptable production strategies, ensures that systems can quickly adjust to changes in demand or resources. Reactive strategies are equally important because they focus on how quickly and effectively a system can respond when unforeseen disruptions occur. Tools such as dynamic scheduling, which adjusts production plans in real time, help minimize downtime in response to issues such as machine failures or material shortages. Having contingency plans and backup resources in place further ensures that production can resume quickly after disruption. A robust resilience plan combines proactive measures, such as forecasting and flexibility, and reactive tools, such as real-time adjustments and recovery plans, creating a manufacturing environment that can withstand and recover swiftly from disruptions.
Making the manufacturing environment more resilient
Creating a more resilient manufacturing environment involves creating a flexible and adaptive system that can respond effectively to both anticipated and unexpected disruptions at different hierarchical levels, that is, macro (supply chain), meso (factory operations), and micro (devices and machines). Although planning-level robustness is essential, true operational resilience is achieved when the physical and digital layers of manufacturing are designed to adapt quickly. For supply chain-level disruptions, such as delayed deliveries, material shortages, or market volatility, manufacturing environments can increase resilience by implementing systems that decouple local production from external dependencies. For example, Katty Fashion has integrated a supply chain digital twin that simulates material delivery delays and workforce fluctuations, allowing factory managers to reschedule batches, redistribute labor, or substitute processes in anticipation of external disruptions. Similarly, Sidenor’s advanced planning tools integrate market signals and raw material pricing data directly into shop floor scheduling logic, enabling proactive reallocation of production resources across multiple facilities.
This transformation relies on embedding reconfigurability directly into the production environment, enabling systems to not only follow updated plans but also autonomously respond to disruptions. For example, GLN Plast has developed a modular injection molding system that allows for rapid swapping of mold inserts, drastically reducing the lead time needed to shift between product variants and improving responsiveness to material changes or market volatility. At the system level, this form of embedded resilience requires the integration of advanced decision support tools with production hardware. In Halcor’s copper tube production, material routing algorithms and part-specific digital twins allow semi-finished materials to be reallocated dynamically based on real-time quality assessments. This not only reduces scrap but also supports continuity under fluctuating supply or specification demand. One of the most effective ways to operationalize resilience is to reduce dependency on human-only reconfiguration decisions. For instance, at Hans Berg, a human assistance system tracks expert tool adjustment patterns and builds a digital knowledge base to guide less-experienced workers through disruption events. This ensures knowledge continuity, which is a critical, but often overlooked, component of environmental resilience.
Environmental resilience also depends on the vertical and horizontal integration of information systems, linking machine-level data with planning tools, and sector-wide indicators. While federated data spaces and asset administration shells enable this technically, the key is aligning workflows such that operators, engineers, and planners respond to the same disruption cues. In Gorenje’s stamping line, for example, ROM-based simulations help assess how design tweaks impact tooling lead-times, supporting better design-to-manufacturing alignment during reconfiguration. A resilient manufacturing environment is not simply automated but is more aware. This includes real-time feedback loops, anomaly detection models tied to reconfigurable responses, and distributed control mechanisms. The goal is not just to recover from disturbances but to continuously adapt with minimal coordination friction. Crucially, embedding resilience into the environment supports not only faster recovery, but also long-term competitiveness. It enables companies to maintain quality and delivery precision despite volatility in labor availability, raw material access, or market demand, all of which were highlighted by pilot partners as recurring challenges.
Resilience and data handling strategies
To strengthen resilience through reconfigurability, manufacturing companies must also design data-handling strategies with multilevel capabilities (see
Table 18). At the macro (supply chain) level, predictive analytics, early detection tools, and resilience assessments align external signals with internal goals. At the meso (factory) level, digital twins, advanced planning, and reconfiguration tools provide insights into actionable operations. At the micro-(machine/device) level, real-time sensing, assistance systems, and edge analytics enable rapid adaptation and autonomous recovery. It is essential to ensure data quality, interoperability, and secure data exchange across these levels. A modular, adaptive data handling architecture with common data models, federated data spaces[8], and plug-in resilience services–enables continuous learning, faster reconfiguration, and sustained operational continuity.
Table 18. Data handling tasks by the scope level.
| Scope level | Data sources | Primary tasks | Typical outcomes |
|---|
| Macro (supply chain) | External signals, supplier data, market indicators, policy alerts. | Resilience assessment, risk scoring, scenario planning, data quality check and improvement. | Upstream adjustments, supplier diversification, buffer/change strategies. |
| Meso (factory) | MES/ERP data, shop-floor sensors, DT, logistics data. | Scheduling optimization, reconfiguration planning, DT-based testing, advanced process control, data quality check and improvement (also for micro level). | Quick line changes, reduced downtime, improved throughput. |
| Micro (machine/device) | Sensor data, machine data and logs, inline quality, condition monitoring data. | Predictive maintenance, process control, anomaly detection, parameter optimization. | Fewer outages, longer tool life, better or stable quality. |
At the macro level (supply chain resilience), the main data-handling activities are to detect and anticipate external disturbances that affect material availability, prices, energy, logistics, and regulations, and then translate external risk signals into robust guidelines for production planning and supplier engagement. The success factor for this is the correct and cost-effective implementation of
• Diversified data streams: macro indicators (i.e., commodity prices, energy costs, exchange rates), transport and logistics signals, supplier risk scores, policy/regulatory alerts, and geopolitical situations.
• The resilience assessment framework quantifies readiness to shocks using a scoring approach (stability, flexibility, change) and a penalty-of-change (PoC) perspective to compare alternate supply chain configurations before disruptions materialize.
• Interoperable data handling and exchange using data spaces (e.g., Gaia-X, IDS) to share risk signals with validated partners while preserving confidentiality.
• Early detection tools and appropriate dashboards: GPT-based or other AI-enabled risk monitors that merge external signals with a company-supply-chain context to generate scaled risk scores and concise rationales for decision-makers.
At the meso level (factory resilience and reconfiguration), the main data-handling activities are to turn macro insights into resilient production plans and rapid reconfiguration of lines, cells, and material flows. As in the previous point, the success factors are the correct and cost-effective implementation of:
• Digital twin of the production system: end-to-end representation of processes, equipment, tooling, and logistics connected via a digital thread (e.g., AAS-based).
• Resilience toolbox: A modular service set including resilience assessment, master production scheduling adjustments, fault detection, and human-assisted decision support.
• Data integration across layers: Connect ERP/MES, shop-floor control, instrumented equipment, and external data spaces to enable cross-layer optimization.
• Scenario-based planning: Simulate disruptions (e.g., machine downtime, material shortfalls, demand shifts) and evaluate alternative configurations, for example, using DT-based optimization.
• Data quality estimation and improvement: ensure time-aligned data, consistent units, complete histories, and traceable data provenance across plants and suppliers.
At the micro level (machine/equipment or device resilience), the main data-handling activities are to detect faults early, optimize tool settings, and adapt operations in real time to maintain continuity and quality. The success factor for this is the correct and cost-effective implementation of
• Sensor and edge data pipelines, that is, continuous collection of vibration, temperature, force, acoustics, and quality measurements; edge processing to filter, detect anomalies, and trigger reconfiguration actions.
• Digital twins at the machine level: model tool wear, process capabilities, and quality outcomes; feedback into maintenance, process, or technology adjustments.
• Tooling and knowledge capture: human-assisted decision systems that learn from historical expert adjustments, store best practices, and guide operators during disruptions or failures.
• Real-time reconfiguration support: automated or semi-automated tool changes, scheduling tweaks, and resource reallocation based on current sensor data and digital twin predictions.
At the same time, high-quality data are the backbone of accurate predictions, reliable resilience scoring, and trustworthy reconfigurations. High-quality data ensure that macro (i.e., external) signals, meso plans, and micro signals can be used for coherent actions. To achieve this, a comprehensive strategy for avoiding data-quality issues must be implemented.26 Ideally, this should be implemented as a data quality framework that includes the definition and monitoring of quality dimensions, such as accuracy, completeness, timeliness, consistency, lineage, and traceability, as well as the implementation of automated data quality checks at the ingestion and processing stages. To achieve this, it is essential to consider the available process knowledge and physical properties of machines or devices.
Discussion – the role of digital tools in increasing resilience
Awareness
Raising awareness among industries regarding digital tools for resilience requires demonstrating their tangible benefits in minimizing disruptions, optimizing resource utilization, and ensuring operational continuity. Real-world case studies show that digital twins, AI-driven services, and federated data spaces have improved adaptability and can build trust in these technologies. Engaging stakeholders through hands-on workshops, pilot programs, and interactive demonstrations will allow companies to experience how digital solutions enhance decision making and flexibility. Additionally, providing clear roadmaps for gradual adoption, starting with small-scale implementations before full integration, can help industries navigate the transition with confidence and ensure long-term resilience in an increasingly complex manufacturing landscape. Among the tools developed in these projects, the GPT-based Early Detection Tool exemplifies how AI can turn heterogeneous, unstructured information (news, legal texts, economic reports) into concrete early warnings and weak-signal dashboards that are directly actionable for European manufacturing companies.
Anticipation
Anticipation of industrial resilience involves proactively identifying potential disruptions before they occur and implementing strategies to mitigate their impact. By leveraging predictive analytics, AI-driven forecasting services, and digital twin simulations, industries can enhance their ability to foresee supply chain bottlenecks, equipment failures, and shifts in market demand. This forward-looking approach allows companies to develop contingency plans, optimize resource allocation, and ensure continuity, even under uncertain conditions. Industries benefit from anticipation by reducing downtime, minimizing financial losses, and improving overall efficiency. Predictive maintenance can prevent unexpected equipment failures, whereas scenario simulations help assess the impact of different disruption scenarios on production and supply chains. In addition, integrating real-time monitoring systems enables businesses to detect early warning signs and respond swiftly. To maximize these benefits, industries must establish data-driven decision-making frameworks and foster a culture of resilience, ensuring that they are prepared to act rather than react when disruptions arise. By providing risk scores and textual rationales days or weeks before disturbances are visible in plant-level KPIs, the Early Detection Tool operationalizes anticipation. It gives planners and engineers enough lead time to run digital-twin scenarios, adjust master production schedules, and prepare reconfiguration options rather than reacting only once a disruption has fully manifested.
Adaptation
Industries can enhance resilience by adopting digital technologies such as AI-driven decision support systems, digital twins, and federated data spaces. However, several challenges must be addressed to ensure a successful implementation. Integration complexity remains a major barrier because many legacy systems are not designed to work seamlessly with modern digital tools. In addition, data silos within companies and across supply chains limit visibility and coordination, making it difficult to respond effectively to disruptions. High initial investment costs, both in terms of technology and workforce training, can slow down adoption, while employee resistance to new tools can further complicate this transition. Moreover, increased data sharing raises concerns regarding cybersecurity and regulatory compliance.
To overcome these challenges, industries should incrementally implement digital tools, starting with small-scale pilot projects before scaling up. Standardized data-sharing practices enabled by federated data spaces can facilitate seamless integration and improve collaboration across supply chains. Training and upskilling programs are essential to ensure that employees can effectively use new technologies and reduce their resistance to change. Cost-effective solutions, such as cloud- and subscription-based models, can lower the financial barriers to adoption. Cybersecurity must be a core consideration from the outset, with robust frameworks in place to protect industrial data. By strategically addressing these challenges, industries can successfully integrate digital solutions to ensure greater adaptability to disruptions and long-term resilience.
Conclusions and insights for policy
From the wide variety of resilience challenges across the various sectors displayed above, the two research and innovation projects, although halfway into completion, we can discern several tendencies that should inform future work aimed at increasing resilience in and/or manufacturing in Europe.
Resilience as a new mode of operations
There is a need to expand the paradigm of ‘just-in-time’ manufacturing with a ‘just-in-case’ resilience response strategy. Although several companies among the use cases presented do have some form of supply chain (risk) monitoring or emergency plans or strategies in place, very few to none have made a connection to either increasing the use of digital tools for risk awareness and anticipation or to direct impacts on shop-floor implications, such as reconfigurability. However, recent crises and the global geopolitical instability that we are currently facing show that resilience –capability is not a nice-to-have, but a necessity. Long-term resilience planning and forecasting, although very difficult to put into practice in industries that mostly deal with short-term planning, can prove lifesaving, especially for smaller companies and fragile supply chains. Tools such as resilience self-assessment and supply chain digital twins represent the first building blocks in a resilience roadmap.
Different levels of measures and tools for reconfigurability and resilience
We present three different levels on which resilience capability can be improved and how they are interlinked. Although full integration of these three layers via digital tools is still in the very early stages, in the pilot lines presented, the goal is to develop digital tools for each layer (macro, meso, micro, or sector, factory, production line/machine) and to connect those layers via most likely edge computing platforms. One of the main challenges (and potential gains) identified by almost all companies involved in these projects was the breaking of silos, and thus data, between departments, and along the value chain. In terms of resilience, improving the information position not only at the factor level, but also at the value and sector levels is a key factor. However, connecting higher-level supply chain prediction or demand data to machine-level reconfigurability data is far from an easy task. Even with the help of AI-based tools in programming or data management, deep production process expertise is needed to understand what data are relevant, for whom, and when. Much more effort and attention will need to be paid to data and information architecture, digital threads, and legacy systems to maximize the added value of digital tools for resilience.
Looking ahead: Short- and long terms challenges
With both project development and integration at industry sites, we identified several key insights and challenges related to resilience and reconfigurability for manufacturing:
• Resilience self-assessment tools are necessary to increase awareness of resilience, but their uptake is scarce. While some companies in our projects have crisis response strategies, stronger ties need to be made to anticipate approaches.
• Resilience awareness and strategies can act as accelerators for data sharing across the value chain (via federated data spaces). As supply chain risk signalling tools de facto touch upon multiple actors along the value chain, safe and secure data sharing is key for further development and improvement of such tools.
• Being able to deal with legacy systems and having a proper data architecture and digital team are key ingredients to ensure useful digitization of all three layers. In all use cases, collecting and using data on the machine, cell, or factory level requires knowledge and expertise on legacy ERP and MES systems and a wide variety of data formats and programming languages.
• There are limits to the sphere of influence of SMEs, and mid-cap companies in manufacturing have globalized supply chains. Recognizing external risks or disruptions is one aspect that can act upon them. More sectorial or regional-level intelligence sharing is needed to better anticipate geopolitical or other shocks and to formulate adequate responses and support long-term transitions and competitiveness.
Ethics and consent
Ethical approval and consent were not required.







